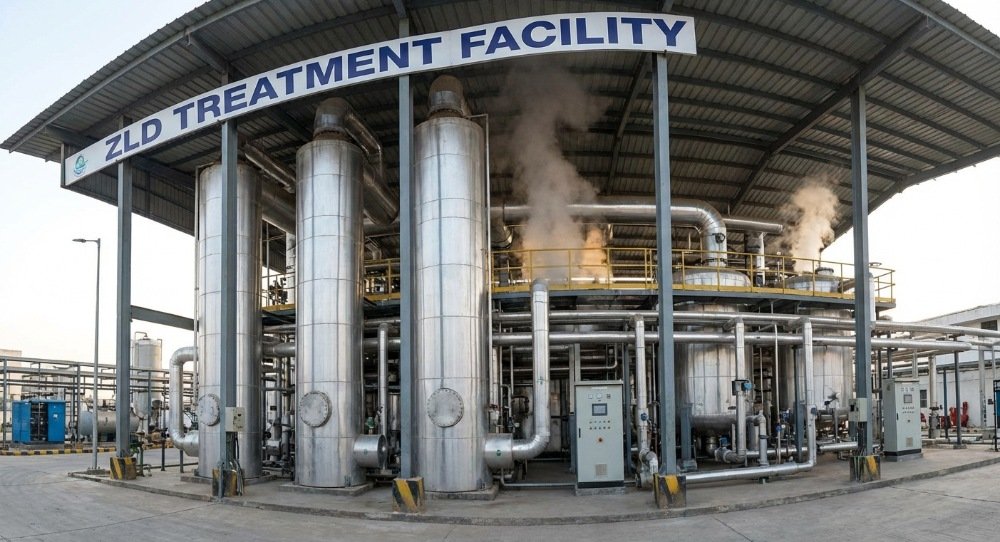
Industrial Wastewater & ZLD
Brine concentration, industrial effluent volume reduction, landfill leachate and selected ZLD pre-concentration or evaporation duties.


A triple effect evaporator reuses vapor from one effect as the heating medium for the next. Compared with a single-effect system, this can substantially reduce live-steam demand while keeping a practical balance between energy use, equipment complexity and capital cost.
Memva configures three-effect evaporation systems around the actual process duty: feed flow, inlet and target concentration, viscosity, boiling-point elevation, fouling tendency, corrosion risk and available utilities. Falling-film, forced-circulation and different feed arrangements can be evaluated according to the material.
The number of effects should be selected from process economics, not from a fixed rule. A three-effect system is commonly considered when continuous evaporation and steam cost are important, but the extra complexity of a larger multi-effect train is not justified.
The key idea is latent-heat reuse. Each downstream effect operates at a lower pressure and boiling temperature, allowing vapor generated in the previous effect to provide useful heating duty.
Live steam supplies the initial heat. Part of the solvent evaporates from the feed.
Vapor from the first effect condenses on the heating side and drives further evaporation at a lower pressure.
Vapor from the second effect provides the next heating duty. The third effect normally runs at the lowest pressure.
Vapor leaving the last effect is condensed. Concentrate is discharged according to the selected feed arrangement.
Feed arrangement affects product temperature history, pumping requirements, viscosity and heat transfer. It should be selected from the fluid properties rather than described as universally “best.”
Feed enters the first effect and moves toward lower-pressure effects in the same general direction as the vapor cascade. Inter-effect liquid transfer can often use the pressure difference.
Often considered for: hot feed and processes where the final concentrated product should remain in the lower-temperature effects.
Feed enters the last effect and is pumped toward the first effect against the pressure gradient. The most concentrated liquor reaches the highest-temperature effect.
Often considered for: cold feed or high-viscosity final concentrate, because the higher final temperature can reduce viscosity and improve heat transfer.
Combines forward and backward routing to balance pumping, temperature history and viscosity. The exact sequence is project-specific.
Often considered for: duties where neither pure forward nor pure backward feed gives the best compromise.
Fresh feed is distributed to multiple effects instead of passing through all effects in sequence.
Often considered for: selected crystallizing or slurry-forming services where solids handling is a primary design issue.
A useful quotation starts with feed data. Capacity alone is not enough to size the heat-transfer area, select circulation mode or estimate steam consumption.
Often evaluated for lower-viscosity, relatively clean liquids where short residence time and efficient heat transfer are important.
Often evaluated for higher-viscosity, fouling, scaling, slurry-forming or crystallizing duties where controlled velocity is important.
Construction material, instrumentation, PLC/HMI functions, cleaning arrangement and remote monitoring should match the process and site standard.
Three-effect evaporation can be applied to wastewater reduction and process concentration, but the heat-exchanger type and circulation method must match the specific fluid.
Brine concentration, industrial effluent volume reduction, landfill leachate and selected ZLD pre-concentration or evaporation duties.
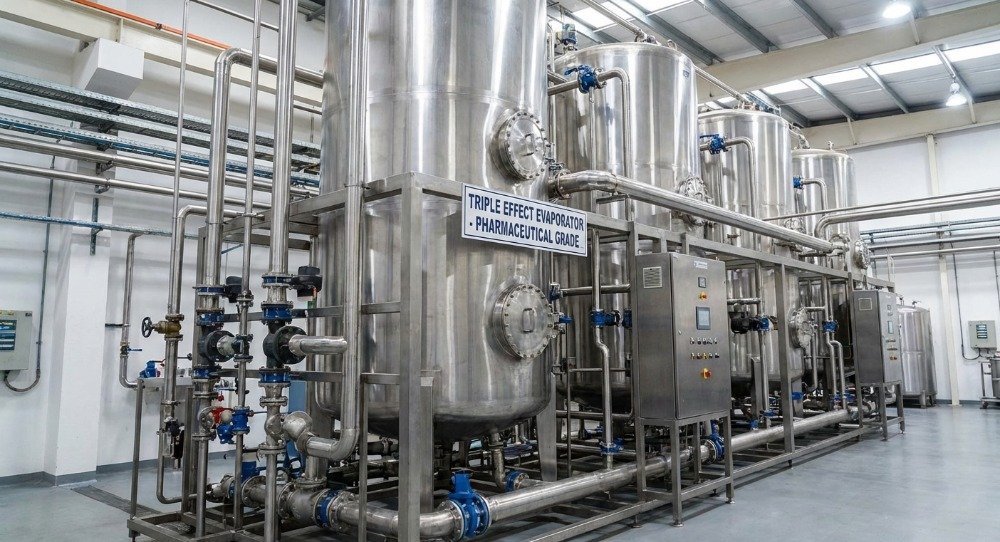
Concentration of compatible process solutions and intermediates where energy use, corrosion and product temperature history are evaluated together.
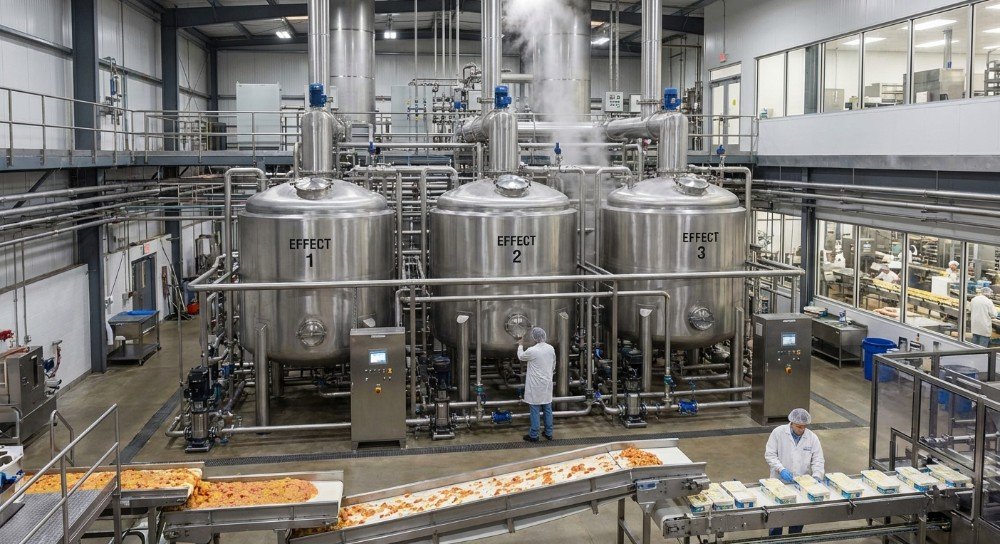
Selected juice, dairy, sweetener and food-process streams, subject to hygiene, residence-time and product-quality requirements.
More effects usually reduce live-steam demand, but they also add heat-transfer area, controls and equipment complexity. MVC/MVR shifts much of the energy requirement from live steam toward electrical compression.
Lower equipment complexity, but typically the highest live-steam demand per kg of water evaporated.
View single effectReuses vapor once. Often evaluated when some steam reduction is needed without the full complexity of three effects.
View double effectReuses vapor across three effects and can be a practical option for continuous duties where steam cost is important.
Evaluate my processCan reduce dependence on live steam, but power price, compressor duty, boiling-point elevation and process stability become key selection factors.
View MVC evaporatorApprox. live steam = water evaporation duty ÷ steam economy
Example: if the required water removal is 10,000 kg/h and the project design reaches a steam economy of 2.5 kg evaporation/kg live steam, the first-pass live-steam estimate is about 4,000 kg/h. This is a screening calculation only; final duty requires a full heat and mass balance.
A fixed online price is rarely meaningful for engineered evaporation equipment. The main cost drivers are evaporation duty, heat-transfer area, metallurgy, circulation method, vacuum system, condenser design, instrumentation, automation, cleaning requirements and project scope.
Water removal rate, concentration target, viscosity and boiling-point elevation determine the core thermal design.
Corrosion-resistant alloys can materially change equipment cost and should be selected from actual chemistry.
Pumps, condenser, vacuum package, CIP, controls, skid/module fabrication, installation support and documentation all affect quotation scope.
If you are still deciding the number of effects or whether to use mechanical vapor compression, compare the related Memva pages before requesting a final configuration.
It is a multiple-effect evaporation system with three sequential effects. Live steam supplies the first effect, vapor from the first effect heats the second, and vapor from the second heats the third. The pressure is reduced from effect to effect so each vapor stream can transfer heat to the next stage.
A useful early design reference is a steam economy around 2.3–2.7 kg of water evaporated per kg of live steam, but actual consumption depends on feed temperature, boiling-point elevation, heat losses, vacuum conditions, fouling and heat-transfer performance. A project heat and mass balance should be used for quotation.
Neither is universally better. Forward feed can reduce inter-effect pumping and keeps the most concentrated liquor in the lower-temperature effects. Backward feed requires pumping toward higher pressure but is often useful for cold feeds or high-viscosity final concentrates because the concentrated liquor reaches the hotter first effect.
It can be considered, but scaling tendency must be evaluated before selecting the exchanger and circulation mode. High-salt, fouling or crystallizing duties may require forced circulation, higher liquid velocity, pretreatment, cleaning provisions or a different evaporation configuration.
Provide feed flow, operating hours, feed temperature, inlet and target concentration, viscosity if available, TDS or dissolved salts, major contaminants, pH/corrosion data, scaling tendency, available steam pressure, cooling-water conditions and required material or site standards.
Vapor recompression can be evaluated as part of a hybrid energy-recovery design. The correct arrangement depends on vapor conditions, compression ratio, electricity and steam costs, boiling-point elevation and the required operating flexibility.
Compare the additional installed cost against annual steam savings under the same evaporation duty and operating hours. Use your actual steam price, utility conditions and maintenance assumptions. A fixed “2–4 year” payback statement is not reliable without those project inputs.
For a useful first evaluation, send the process data below. Even partial data is better than only sending a target capacity.
Use the form below and include as much feed information as possible.