

Lorem ipsum dolor sit amet, consectetur adipiscing elit. Ut elit tellus, luctus nec ullamcorper mattis, pulvinar dapibus leo.
Memva designs mechanical vapor compression and mechanical vapor recompression evaporator systems for high-salinity industrial wastewater, brine concentration, water recovery and Zero Liquid Discharge applications.
An MVC/MVR evaporator recovers the energy contained in generated vapor instead of continuously relying on fresh heating steam. The vapor is mechanically compressed, its saturation temperature is increased, and it is reused as the heating medium for further evaporation.
For industrial wastewater projects, the correct system design depends not only on treatment capacity, but also on wastewater chemistry, scaling tendency, boiling-point rise, corrosion, condensate quality and the required final concentration.
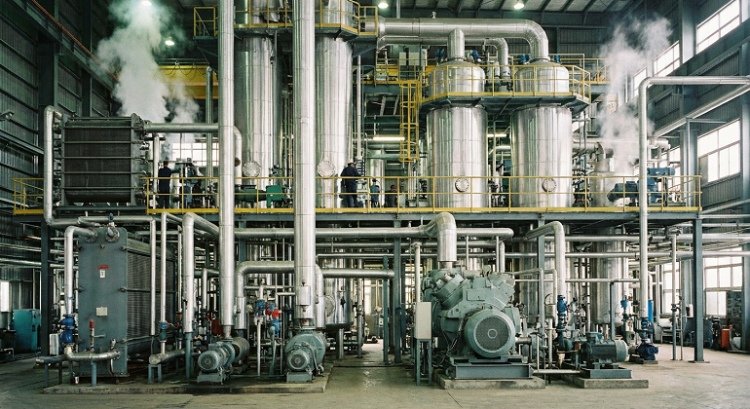
An MVC evaporator uses mechanical compression to raise the pressure and saturation temperature of vapor generated during evaporation. The compressed vapor is then returned to the heat-transfer surface, where it condenses and releases latent heat for continued evaporation.
In industrial evaporation, this principle is also commonly referred to as Mechanical Vapor Recompression (MVR). For this reason, the terms MVC evaporator and MVR evaporator are often used when discussing energy-recovery evaporation systems.
During stable operation, most of the thermal energy is circulated within the system. Electricity is mainly required for the vapor compressor, pumps, instrumentation and auxiliary equipment. Depending on the process configuration, an external heat source may still be required during startup or to compensate for heat loss.
A reliable MVC/MVR design must also evaluate salt composition, scaling tendency, foaming, viscosity, volatile contaminants, corrosion, boiling-point rise, final concentration and the required condensate quality.
High TDS alone does not determine whether an evaporator is the right treatment process. Feed chemistry, disposal cost, water reuse requirements and the final ZLD route should be evaluated together.
The process forms a thermal energy loop by recovering the latent heat contained in vapor generated from the wastewater itself.
Wastewater enters the treatment system and is brought toward the required evaporation temperature using available process heat where practical.
Water is evaporated from the circulating feed, increasing the concentration of dissolved and suspended non-volatile components.
Generated vapor is separated from entrained liquid droplets before it enters the vapor compression stage.
The vapor compressor increases vapor pressure and saturation temperature, creating the temperature difference required for heat transfer.
Recompressed vapor condenses on the heating side of the evaporator and transfers its latent heat back to the circulating wastewater.
The system produces recovered condensate and a reduced-volume concentrate. Their downstream treatment depends on the water reuse, discharge or ZLD target.
The final equipment configuration should be selected from the actual wastewater characteristics and evaporation duty rather than using one fixed design for every application.
Provides the heat-transfer area required to transfer energy from recompressed vapor to the wastewater while maintaining suitable circulation conditions.
Separates generated vapor from entrained liquid droplets before compression. Separator and demister performance also influence condensate quality.
Raises vapor pressure and saturation temperature so that the vapor can be reused as a heating medium. Compressor selection depends on vapor flow, required temperature lift and process conditions.
Maintain the flow conditions needed for stable heat transfer, concentration control and wastewater circulation.
Cleaning frequency and chemical cleaning strategy should be selected according to the expected scaling, fouling and wastewater chemistry.
Instrumentation and automatic control maintain process conditions and provide operating data, alarms, interlocks and protection for critical equipment.
Send us your wastewater flow rate, water analysis and treatment target. Memva can evaluate whether evaporation should be used directly or combined with membrane concentration, crystallization or other treatment stages.
Two wastewater streams with the same daily flow can require very different evaporator configurations. These are the main parameters considered during process design.
Average and peak flow in m³/day or m³/h, operating hours per day and expected load variation determine the required evaporation capacity.
Total dissolved solids alone are not sufficient. Chloride, sulfate, calcium, magnesium, silica and other ions affect scaling, corrosion and achievable concentration.
Organic matter, ammonia, solvents and surfactants may affect foaming, heat-transfer performance and condensate quality.
The design should define the required volume reduction, final concentrate composition and whether downstream crystallization or solids separation is required.
Required discharge or reuse quality determines whether condensate can be reused directly or requires additional polishing treatment.
Chloride concentration, temperature, pH and wastewater chemistry must be considered when selecting stainless steel, duplex stainless steel, titanium or other corrosion-resistant materials.
Available electrical supply, startup heat source, cooling utilities, installation space and local plant conditions influence system configuration.
Expected precipitation and fouling behavior influence circulation mode, operating concentration, cleaning frequency and maintenance accessibility.
A universal electricity consumption figure such as “15–40 kWh per m³ of wastewater” should not be used as a guaranteed value for every project. Actual consumption depends on evaporation duty, boiling-point rise, temperature lift, compressor efficiency, feed temperature and final concentration.
Send your wastewater analysis and required treatment capacity to obtain a project-specific energy estimate.
MVC/MVR evaporation can be used as a standalone concentration stage or as part of an integrated membrane, evaporation and crystallization treatment process.
Concentration of wastewater containing high levels of dissolved salts when biological or membrane treatment alone cannot achieve the required volume reduction.
Further concentration of membrane reject after osmotic pressure, scaling risk or recovery targets limit additional membrane concentration.
Thermal concentration before crystallization, salt separation or final solids handling in a ZLD treatment train.
Concentration of selected chemical wastewater streams where salt composition, organics, corrosion and scaling require project-specific process design.
Volume reduction and water recovery from selected high-salinity process streams generated during mining, refining and metal processing.
Concentration and water recovery for selected high-TDS process wastewater generated during battery material and new-energy manufacturing.
Thermal concentration may be considered for difficult wastewater after volatile components, COD, foaming behavior and condensate treatment requirements are evaluated.
Concentration of dissolved components where downstream crystallization, salt recovery or process-water reuse forms part of the overall treatment objective.
Generated vapor is recompressed and reused as the heating medium, reducing continuous dependence on fresh heating steam during stable operation.
Evaporation removes water from the wastewater and produces a smaller concentrate volume for further treatment, crystallization or disposal.
Condensate can potentially be reused within the plant, subject to feed composition, volatile contaminants and the required reuse-water quality.
MVC/MVR evaporation can be integrated with membrane concentration and crystallization to form a complete Zero Liquid Discharge treatment route.
PLC/HMI controls can automate temperature, pressure, circulation, liquid level and equipment protection for continuous industrial operation.
Wetted parts can be selected according to chloride level, temperature, pH and corrosion conditions instead of relying on a single material specification for all wastewater.
These technologies are not always direct competitors. In many wastewater and ZLD projects, membrane concentration and evaporation are used together to reduce total treatment cost.
Continuous thermal concentration of high-salinity wastewater where vapor heat recovery is attractive.
Primarily electricity for vapor compression during stable operation.
Boiling-point rise, compressor temperature lift, scaling, corrosion and wastewater chemistry.
Thermal concentration where steam is readily available and multiple effects can improve steam economy.
Steam plus electrical power for pumps and auxiliary equipment.
Number of effects, available steam, temperature profile, heat-transfer area and installation space.
Membrane concentration of difficult wastewater before thermal evaporation where feed chemistry and osmotic pressure allow.
Electricity for high-pressure feed pumping.
Osmotic pressure, recovery, membrane rejection, fouling, scaling and concentrate disposal route.
Pretreatment → membrane concentration → MVC/MVR evaporation → crystallization or solids separation.
The exact treatment route should be selected from wastewater chemistry and overall lifecycle cost rather than from a single technology preference.
For industrial wastewater equipment, flow rate alone is not enough to prepare a reliable evaporator design. Send as much of the following information as you currently have.
Average and maximum flow rate in m³/day or m³/h, operating hours per day and expected production variation.
TDS, COD or TOC, pH, chloride, sulfate, calcium, magnesium, silica, ammonia and any known process chemicals.
Tell us whether the feed is raw wastewater, RO concentrate, DTRO concentrate, mother liquor or another process stream.
Required volume reduction, water recovery, final concentrate target, discharge requirement and whether crystallization or ZLD is required.
Electrical supply, available steam or startup heat source, installation environment and any plant utility limitations.
Memva develops industrial wastewater treatment systems around the actual characteristics of each wastewater stream rather than selecting an evaporator only by nominal flow rate.
Depending on the project, the treatment process may combine membrane concentration, MVC/MVR evaporation, condensate polishing, crystallization and solids handling to achieve the required wastewater reduction or water-reuse target.
When evaluating an evaporator supplier, compare feed conditions, evaporation load, actual condensate quality, final concentration, installed materials, energy consumption and long-term operating performance whenever project data is available.
In industrial evaporation, both terms are used for mechanical vapor compression and heat-recovery concepts. MVR stands for Mechanical Vapor Recompression and describes the recompression and reuse of generated vapor. Some equipment suppliers use MVC, Mechanical Vapor Compression, for the same or closely related evaporation principle.
It is used to remove water from industrial process streams and wastewater, producing a smaller-volume concentrate and recovered condensate. Typical applications include high-salinity wastewater, brine concentration, membrane concentrate and ZLD systems.
Yes. High-salinity wastewater is a common application, but the design must consider the actual salt composition, boiling-point rise, scaling tendency, corrosion, viscosity and final concentration target.
Yes. Thermal evaporation is often considered after membrane concentration reaches its practical recovery limit. The membrane stage can reduce the hydraulic load before evaporation, while MVC/MVR can further reduce concentrate volume.
Condensate may be suitable for reuse, but this depends on feed composition and the required water quality. Ammonia, volatile organic compounds, foaming or liquid entrainment can affect condensate quality, so polishing treatment may be required.
There is no reliable universal kWh/m³ value for all wastewater streams. Electricity consumption depends on evaporation duty, boiling-point rise, temperature lift, compressor efficiency, feed temperature, concentration target and other process conditions.
During stable operation, recompressed process vapor supplies most of the required evaporation heat. Depending on system configuration, an auxiliary heating source may still be used during startup and to compensate for process heat loss.
Scaling control starts with wastewater chemistry. Circulation mode, operating concentration, temperature, pretreatment, antiscalant strategy where applicable and CIP procedures should be selected according to the salts expected to precipitate.
Maintenance requirements depend mainly on scaling, fouling, compressor configuration, wastewater chemistry and operating concentration. A properly designed system should provide accessible heat-transfer surfaces, appropriate CIP provisions and protection for critical rotating equipment.
Material selection depends on wastewater chemistry, chloride level, pH, operating temperature and corrosion risk. Stainless steel, duplex stainless steel, titanium or other corrosion-resistant materials may be considered depending on the application.
Yes. MVC/MVR evaporation can be used as the thermal concentration stage of a ZLD system, commonly after pretreatment or membrane concentration and before crystallization or final solids separation.
Start with wastewater flow rate, operating hours, TDS, pH, COD or TOC, major dissolved salts, chloride, sulfate, hardness, silica, ammonia, known organic compounds and the required final concentration or water-reuse target.
Tell us what wastewater you need to treat. Feed chemistry and treatment target determine the correct evaporation process and equipment configuration.
If you already have a laboratory water analysis, include it with your inquiry. Even incomplete data can be used for an initial technical discussion.