

Treating saltwater in an industrial setting comes down to one decision: how much water you remove, and how much salt you leave behind. Most plants I work with fall into two groups — those treating brackish process streams at 3,000–35,000 mg/L TDS, and those dealing with true brine above 50,000 mg/L. The first group usually gets by with membranes. The second group almost always needs evaporation, and sometimes a full zero liquid discharge (ZLD) train. In this article I’ll walk through the methods, where each one makes sense, what drives capital and operating cost, and the maintenance issues that actually bite you in year two.

What Makes Saltwater Hard to Treat
Salinity itself isn’t the hard part. Osmotic pressure is. At 35,000 mg/L TDS, you need roughly 27 bar just to overcome the feed’s natural resistance to reverse osmosis. At 70,000 mg/L, you’re looking at 55–70 bar, which is why seawater RO membranes are built differently and why standard brackish elements fail fast in that service.
The second problem is scale. Calcium, magnesium, barium, strontium, silica, and sulfate all become less soluble as you concentrate. A stream that runs clean at 10,000 mg/L can drop scale on a heat exchanger within days at 200,000 mg/L.
The third is variability. I’ve seen plants where TDS swings 40% between shifts because a batch reactor dumps at irregular intervals. Design for the average and you’ll be cleaning membranes every week.
Typical Feed Categories
| Stream type | Typical TDS range | Main treatment path |
|---|---|---|
| Brackish process water | 3,000–15,000 mg/L | RO, sometimes with softening |
| Coal or mine drainage | 5,000–40,000 mg/L | Pretreatment + RO or thermal |
| Seawater / estuarine intake | 30,000–45,000 mg/L | Seawater RO at 55–70 bar |
| Produced water | 20,000–200,000 mg/L | Thermal or hybrid |
| Landfill leachate | 5,000–60,000 mg/L | Biological + membrane + evaporation |
| Concentrate / brine | 50,000–300,000 mg/L | MVC, MVR, or multi-effect evaporation |
Those ranges are indicative. Real numbers depend on your site, your process chemistry, and how much upstream recovery you already have. I’ve seen “brackish” wells at 38,000 mg/L and “brine” that was mostly organic with modest salt.
The Main Methods, Ranked by Where They Fit
Reverse Osmosis and High-Pressure RO
RO is the workhorse for anything under about 45,000 mg/L. Energy use is reasonable, the technology is well understood, and you can scale it in modules. The catch is concentrate. A single-pass RO at 75% recovery still leaves you with 25% of the feed as brine at roughly four times the original salinity. That brine has to go somewhere.
For higher-salinity feeds, high-pressure RO pushes the practical limit. Disc-tube RO (DTRO) is the version I recommend most often for challenging streams because the open channel handles suspended solids and scaling better than spiral-wound elements. If your feed has any biological activity or fine particulates, DTRO will save you a lot of cleaning cycles.
A typical two-stage RO on brackish feed runs 70–85% recovery. On seawater, expect 35–50% without a second pass. Those aren’t targets to brag about — they’re limits you design around.
Evaporation: MVC, MVR, and Multi-Effect
Once you’re above roughly 50,000 mg/L, or once the stream has enough organics that membranes foul constantly, evaporation becomes the practical answer. The three main configurations are:
- Mechanical vapor compression (MVC/MVR) — a compressor recompresses the vapor and reuses its latent heat. Power-hungry on the front end but very efficient in steady state. Best for medium-to-large flows where electricity is affordable.
- Multi-effect evaporation — steam drives the first effect, and each subsequent effect runs on the vapor from the previous one. Two or three effects are common. Steam cost dominates, so this wins where you have cheap waste steam.
- Single-effect evaporation — simple, robust, and usually reserved for small flows or pilot-scale work.
The choice between MVC and multi-effect is mostly an energy-price question. If your plant has waste steam, multi-effect will usually beat MVC on operating cost. If electricity is cheap and steam isn’t available, MVC wins. I’ve seen both configurations pay off, and I’ve seen both fail — usually because someone picked the wrong one for the site’s actual utility profile.
Zero Liquid Discharge
ZLD is not a single technology — it’s a system. Typically it’s RO or DTRO for bulk concentration, then an evaporator to drive the brine close to saturation, then a crystallizer or spray dryer to convert the remaining liquid into a solid you can landfill or sell. Some designs use a brine concentrator followed by a crystallizer; others skip the crystallizer and send concentrated brine to a lined pond, which is cheaper but has its own long-term liabilities.
ZLD makes sense when discharge permits are unavailable, when the receiving water is protected, or when the salt has resale value. It rarely makes sense on cost alone. A well-designed ZLD train typically runs two to four times the capital cost of a conventional RO system and consumes meaningfully more energy per cubic meter treated.
Cost: What Actually Drives the Number
I get asked for a single price per cubic meter all the time, and I always push back. The honest answer is a range, and the range is wide because the variables matter more than the technology.
| Cost driver | Why it matters | Typical impact |
|---|---|---|
| Feed TDS and chemistry | Determines membrane pressure, evaporator size, scaling risk | 2–4x swing in capex |
| Flow rate | Drives equipment size and modular vs. custom build | Economies of scale above 50 m³/h |
| Recovery target | Higher recovery = more concentration stages = more cost | Steep curve above 90% |
| Discharge or ZLD | ZLD adds evaporator + crystallizer + solids handling | 2–4x total capex |
| Energy source | Steam vs. electricity changes opex profile | 30–60% of opex |
| Site conditions | Indoor/outdoor, altitude, ambient temp, corrosion class | 10–25% of capex |
As a rough planning figure — and I want to be clear this is project-dependent, not a quote — a mid-size industrial RO system on brackish feed might land in the low-to-mid six figures in USD for equipment. An MVC evaporator of comparable capacity typically runs higher, and a full ZLD train higher still. Operating cost per cubic meter is usually dominated by electricity or steam, then chemicals, then membrane or mechanical replacement.
The mistake I see most often is optimizing capex. A system that saves 15% on equipment but consumes 25% more energy will lose that savings in eighteen months. Look at five-year total cost of ownership, not the purchase order.
Design Choices That Decide Whether the Plant Runs Smoothly
Pretreatment Is Not Optional
Every membrane and every evaporator is only as good as what’s in front of it. For RO, that means:
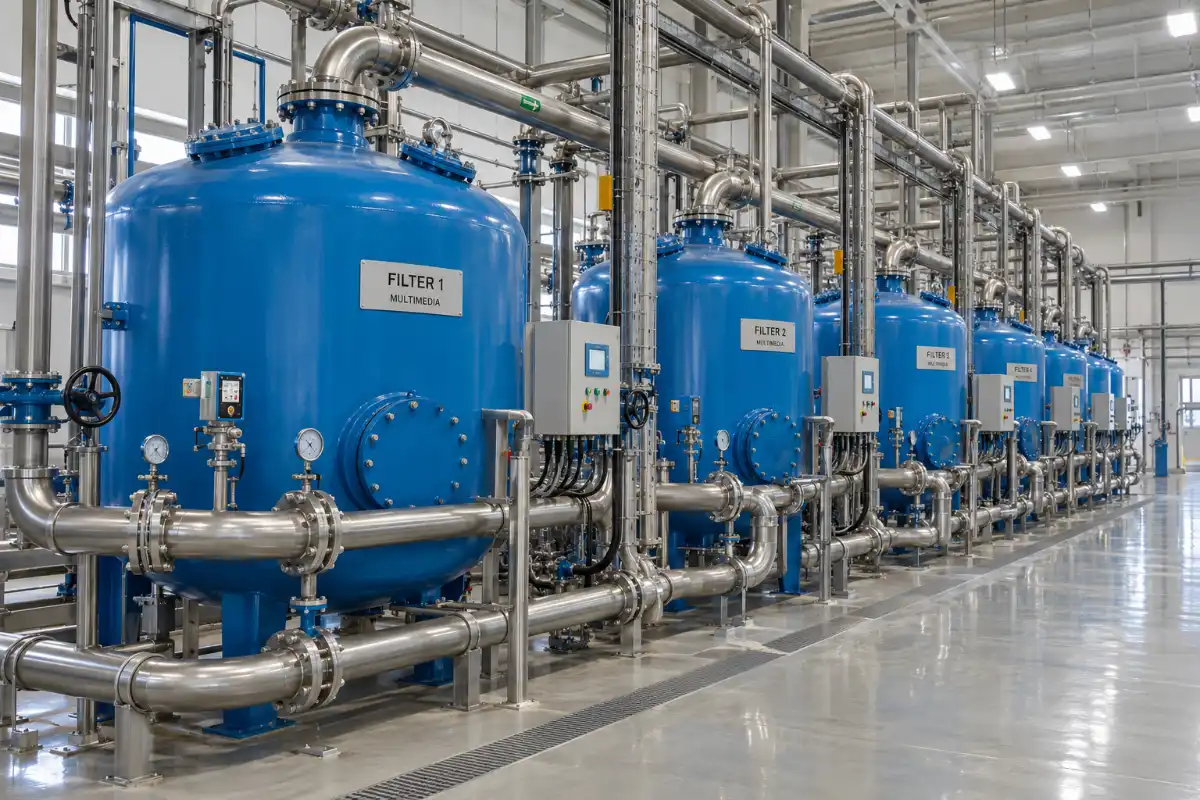
- Coarse and fine filtration to protect the elements
- Antiscalant dosing sized to the actual saturation indices, not a rule of thumb
- Softening or lime softening when hardness is high
- Dechlorination if the feed has free chlorine and you’re using polyamide membranes
- Cartridge filtration as a final barrier
For evaporators, pretreatment usually means removing oil, grease, and volatile organics that would otherwise carry over into the condensate. If your condensate has to meet a discharge limit, this is where you win or lose.
Materials and Corrosion
Chlorides eat carbon steel. At high salinity and elevated temperature, you’re choosing between duplex stainless, super duplex, titanium, and various high-nickel alloys. The right answer depends on chloride concentration, temperature, and whether oxygen is present. I’ve watched a project save money on 316L and replace the entire tube bundle within two years. That’s not a saving.
Redundancy and Turn-Down
Industrial saltwater treatment rarely runs at a constant rate. Design the system to turn down gracefully — variable frequency drives on pumps, multiple smaller evaporator effects rather than one large one, and enough storage to buffer between shifts. A plant that can only run at 100% is a plant that will be bypassed the moment production changes.
Maintenance: The Realistic Picture
Here’s what a well-run system actually needs, based on what I’ve seen across dozens of installations:
- Daily: pressure differentials, conductivity, flow rates, and a visual check on any obvious leaks or vibration.
- Weekly: antiscalant and chemical dosing verification, compressor oil checks on MVC units, and cleaning cycle logs.
- Monthly: membrane performance normalization, heat exchanger inspection, and calibration of critical instruments.
- Annually: membrane replacement planning, evaporator tube inspection, compressor overhaul on MVC, and a full system performance review.
The single biggest maintenance cost in most plants is membrane replacement. RO elements typically last two to five years depending on feed quality and cleaning discipline. Evaporator heat exchangers last much longer if scaling is controlled, but a single scaling event can cost you a week of downtime and a bundle of cleaning chemicals.
If you want a deeper look at how heat exchanger design affects long-term reliability in these systems, the heat exchanger selection guide covers the trade-offs in detail.
Common Failure Modes and How to Avoid Them
Membrane Fouling and Scaling
Almost always a pretreatment or dosing problem. If your antiscalant is dosed by a timer instead of a flow-proportional pump, you’re guessing. Fix the dosing first, then look at the membranes.
Evaporator Scaling
Calcium sulfate, calcium carbonate, and silica are the usual suspects. Silica is the hardest to manage because it doesn’t respond to conventional antiscalants the way hardness does. If your feed has more than about 100 mg/L silica, plan for either elevated temperature operation, seeding, or a pretreatment step that removes it.
Compressor Failures on MVC
Usually caused by carryover — liquid droplets reaching the compressor. A properly sized mist eliminator and a stable liquid level solve most of this. When they fail, the repair bill is significant and lead times can be long.
Condensate Quality Drift
If your condensate is going to discharge or reuse, watch it. Volatile organics, ammonia, and fine droplets all find their way through. A polishing RO or activated carbon step on the condensate is cheap insurance.
When to Bring in Evaporation, and When Not To
I use a simple rule. If the feed is under 45,000 mg/L and doesn’t have heavy organic loading, start with membranes. If it’s over 50,000 mg/L, or if membranes foul faster than you can clean them, go straight to evaporation. If you need ZLD, plan the full train from day one — retrofitting a crystallizer onto a system that wasn’t designed for it is expensive and awkward.
For systems where the flow is small but the salinity is high, single-effect evaporation can be the right answer. For medium flows, MVC or MVR usually wins on operating cost. For large flows with available waste steam, multi-effect evaporation is often the most economical.
If you’re working through which configuration fits your site, the MVC evaporator overview walks through the operating principles and where the technology earns its keep.
My rule of thumb after fifteen years: design for the worst feed you can reasonably expect, not the average. The average never shows up on the day the permit inspector does.
Putting It Together: A Project-Style Example
A metal finishing plant I worked with had a rinse water stream at roughly 8,000 mg/L TDS, but with heavy metals and a pH that swung between 3 and 10 depending on the process line. The original plan was straight RO, but the membranes were fouling within two weeks.
We restructured it: pH adjustment and metals precipitation first, then multimedia filtration, then DTRO for bulk concentration, and finally a small MVC evaporator to handle the DTRO concentrate. Recovery went from an unworkable 40% to a stable 92%, and membrane cleaning dropped from weekly to quarterly.
The capex was higher than the original design. The five-year cost was lower, and the plant stopped getting notices from the local authority. That’s the trade-off most projects actually face.
If you’re at the point where you need to size equipment or compare configurations for your specific stream, it’s worth talking through the numbers before committing. You can reach our engineering team here to walk through your feed analysis and recovery targets.
Frequently Asked Questions
How do I choose between RO and evaporation for saltwater?
Start with feed TDS and organic content. Under 45,000 mg/L with low organics, RO or DTRO is usually the right first step. Above 50,000 mg/L, or when membranes foul faster than you can clean them, go to evaporation. The crossover point isn’t fixed — it depends on your specific chemistry and how much pretreatment you’re willing to run.
What is the typical energy consumption for an MVC evaporator?
It varies widely with the feed and the design, but MVC systems generally consume somewhere in the range of 15–40 kWh per cubic meter of distillate produced. The number depends on boiling point elevation, compressor efficiency, and how much heat recovery the design includes. Always ask for a specific energy calculation based on your feed analysis, not a generic figure.
How often do RO membranes need to be replaced in saltwater service?
Two to five years is typical for well-maintained systems. Seawater and high-fouling streams tend to be on the shorter end. If you’re replacing membranes more often than that, the problem is almost always upstream — pretreatment, dosing, or operating pressure outside the design window.
Can I retrofit a ZLD system onto an existing RO plant?
Sometimes, but it’s rarely clean. The RO concentrate stream has to be compatible with the evaporator’s design, and the existing plant may not have the space, utilities, or electrical capacity for the added equipment. It’s usually cheaper to design the full train from the start than to bolt on a crystallizer later.
What causes foaming in evaporators treating saltwater?
Usually surfactants, oils, or high concentrations of dissolved organics in the feed. Antifoam helps short-term, but the real fix is upstream removal — oil-water separation, DAF, or activated carbon depending on what’s in the stream. Foaming that isn’t addressed will eventually cause carryover and contaminate your condensate.
How do I control scaling in a high-salinity evaporator?
Three levers: keep the concentration factor below the saturation point of the worst scalant, operate at a temperature that keeps solubility high, and use antiscalants or seeding where appropriate. Silica is the hardest to manage and often forces a lower concentration factor or a pretreatment step. Get a proper solubility analysis before finalizing the design.
What’s the difference between MVC and MVR evaporators?
In practice, very little — the terms are often used interchangeably. Both use a mechanical compressor to recompress vapor and reuse its latent heat. Some engineers reserve MVR for larger systems and MVC for smaller ones, but the operating principle is the same. What matters is compressor type, turndown capability, and how well the system handles your specific feed.
How much space does a full saltwater treatment train need?
It depends heavily on flow rate and whether you’re including ZLD. A basic RO skid for 20 m³/h might fit in a shipping container footprint. A full ZLD train with evaporation and crystallization can need several hundred square meters, plus height for the evaporator vessel and access for maintenance. Plan for at least 30% more space than the equipment footprint suggests.
Do I need a pilot test before full-scale design?
For any stream above 30,000 mg/L TDS, or any stream with unusual chemistry, yes. Pilot testing reveals scaling behavior, fouling rates, and actual recovery limits that bench data can’t predict. It costs money upfront and saves multiples of that in avoided redesign. I’ve never regretted running a pilot; I’ve regretted skipping one.