

A triple-effect evaporator typically costs between $180,000 and $1.2 million installed, depending on evaporation capacity, materials of construction, and whether it ships as a skid or a field-erected system. The equipment itself usually runs 45–60% of that figure, with the balance going to civil work, piping, instrumentation, and commissioning. If you’re comparing quotes and the numbers are far apart, the difference almost always comes down to heat exchanger surface area, wetted metallurgy, and how much automation the vendor has priced in. In this guide I’ll walk through what actually drives triple-effect evaporator price, how to size one correctly, and where I’ve seen projects go wrong.
What a Triple-Effect Evaporator Actually Does
A triple-effect evaporator uses the vapor boiled off in one vessel to heat the next. You feed steam into the first effect, the vapor it produces drives the second, and the vapor from the second drives the third. The result is roughly three pounds of water evaporated per pound of steam, compared to about one pound in a single-effect unit.
That steam economy is the whole point. On a site where you’re paying for boiler steam, the fuel savings compound quickly. On a site where you have waste heat available, the calculus changes and a triple-effect may not be the right answer at all.
The trade-off is temperature. Each effect runs at a lower pressure and temperature than the one before it, so by the third effect you may be boiling at 60–70°C or lower. For heat-sensitive streams — certain pharmaceutical intermediates, some food products — that’s a problem. For brine concentration and most industrial wastewater, it’s fine.
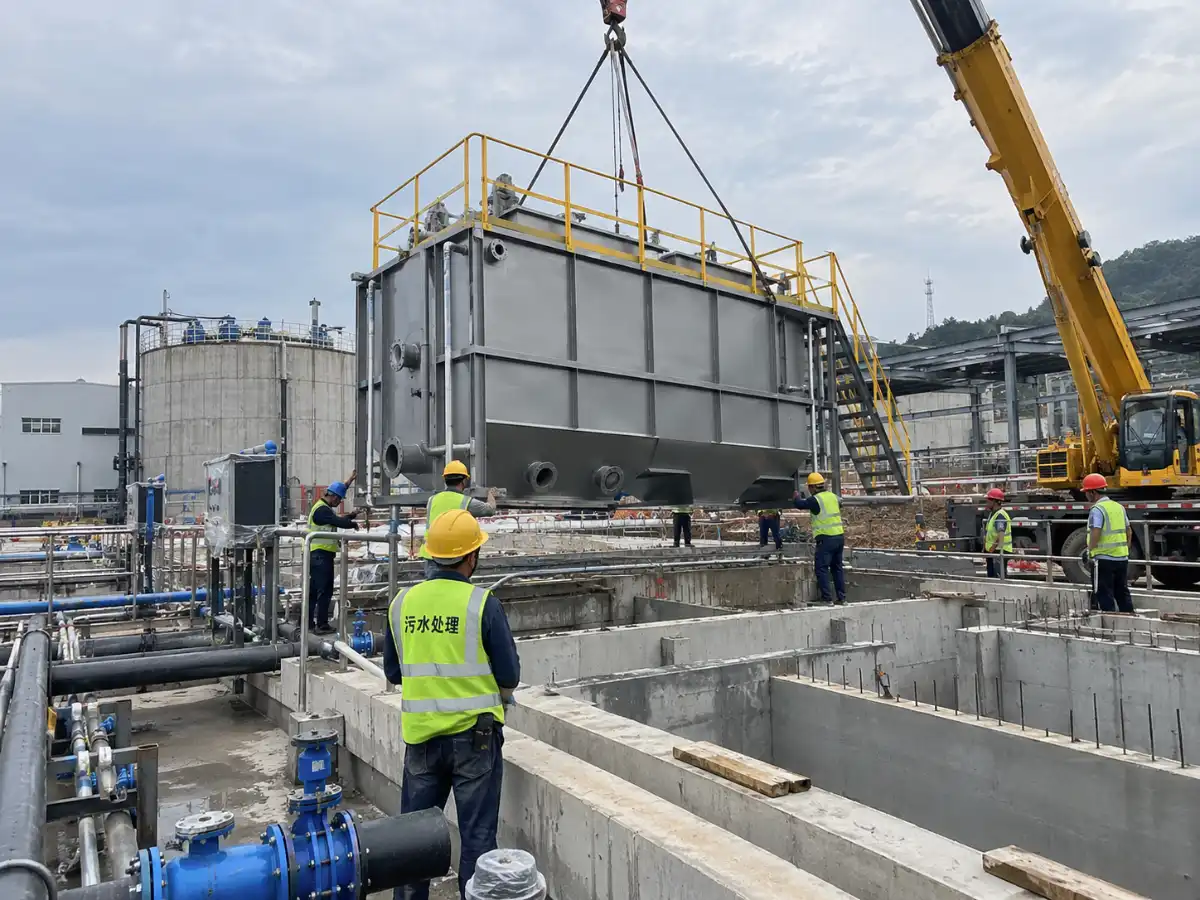
The Price Breakdown: Where Your Money Goes
I’ve reviewed hundreds of evaporator quotations over the years, and the line items are remarkably consistent. Here’s how a typical triple-effect system for industrial wastewater breaks down:
| Cost Component | Share of Total Installed Cost | What Drives It |
|---|---|---|
| Heat exchangers / calandrias | 25–35% | Surface area, tube material (316L, duplex, titanium) |
| Vessels and separators | 12–18% | Diameter, pressure rating, corrosion allowance |
| Vacuum system | 8–12% | Steam ejectors vs. liquid ring pumps |
| Pumps and circulation | 6–10% | Flow rate, solids handling, seal type |
| Instrumentation and controls | 8–14% | PLC vs. DCS, analyzer count, redundancy |
| Piping, valves, insulation | 10–15% | Alloy selection, layout complexity |
| Structural / civil | 5–12% | Skid-mounted vs. field-erected |
| Engineering and commissioning | 6–10% | Project schedule, site conditions |
Notice that heat exchanger surface dominates. This is why two vendors quoting the same evaporation duty can be 40% apart — one sized the exchangers with a conservative fouling factor, the other didn’t. The conservative quote costs more upfront but often pays back within two years on a scaling stream.
Materials are the second big swing. Going from 316L stainless to duplex 2205 can add 20–30% to the wetted cost. Titanium can add 60% or more. On chloride-bearing wastewater, you don’t have much choice.
How Capacity and Concentration Drive Cost
Evaporator cost doesn’t scale linearly with flow. It scales roughly with the amount of water you need to remove, adjusted for how concentrated the feed already is.
A system evaporating 5 tons per hour of water might land in the $350,000–$550,000 range. Double that to 10 t/h and you’re looking at $600,000–$900,000 — not double, because vessels, controls, and civil work don’t double. But the heat exchangers and vacuum system do scale fairly directly.
Feed concentration matters just as much. If your feed is already at 10% dissolved solids and you’re concentrating to 30%, you’re removing a lot of water per unit of product. If you’re feeding at 2% and concentrating to 25%, the duty is much larger for the same product output.
I always ask for three numbers before I’ll even sketch a budget: feed flow, feed concentration, and target concentrate concentration. Without those, any price you get is a guess.
Triple-Effect vs. Alternatives: A Selection Framework
Triple-effect isn’t automatically the right choice just because you want good steam economy. Here’s how I think about it:
| Configuration | Steam Economy (kg evap / kg steam) | Best Fit | Relative Capex |
|---|---|---|---|
| Single-effect | ~0.9 | Small flows, high fouling, waste heat available | Lowest |
| Double-effect | ~1.7 | Moderate flows, moderate steam cost | Low-medium |
| Triple-effect | ~2.5 | Larger flows, high steam cost, thermally stable feed | Medium |
| Multi-effect (4–6) | 3.2–5.0 | Very large flows, cheap steam, low scaling | Medium-high |
| MVC / MVR | 10–25 (as electrical equivalent) | High electricity-to-steam price ratio, steady operation | High |
The rule of thumb I use: if steam costs less than about $12–15 per ton and you have a stable, low-fouling stream above 10 t/h evaporation, a triple-effect is usually the sweet spot. If steam is expensive or you’re paying a lot for boiler fuel, mechanical vapor recompression starts to win despite the higher capital cost.
If your site has cheap waste heat — say from a nearby process or a turbine exhaust — a single or double-effect unit running on that heat can beat a triple-effect running on purchased steam. Don’t assume more effects is always better.
I’ve seen a project where the client insisted on a triple-effect because “three is better than two.” Their steam was essentially free from a neighboring process. They spent an extra $280,000 on the third effect and never recovered it. The right answer was a single-effect unit using the waste heat.
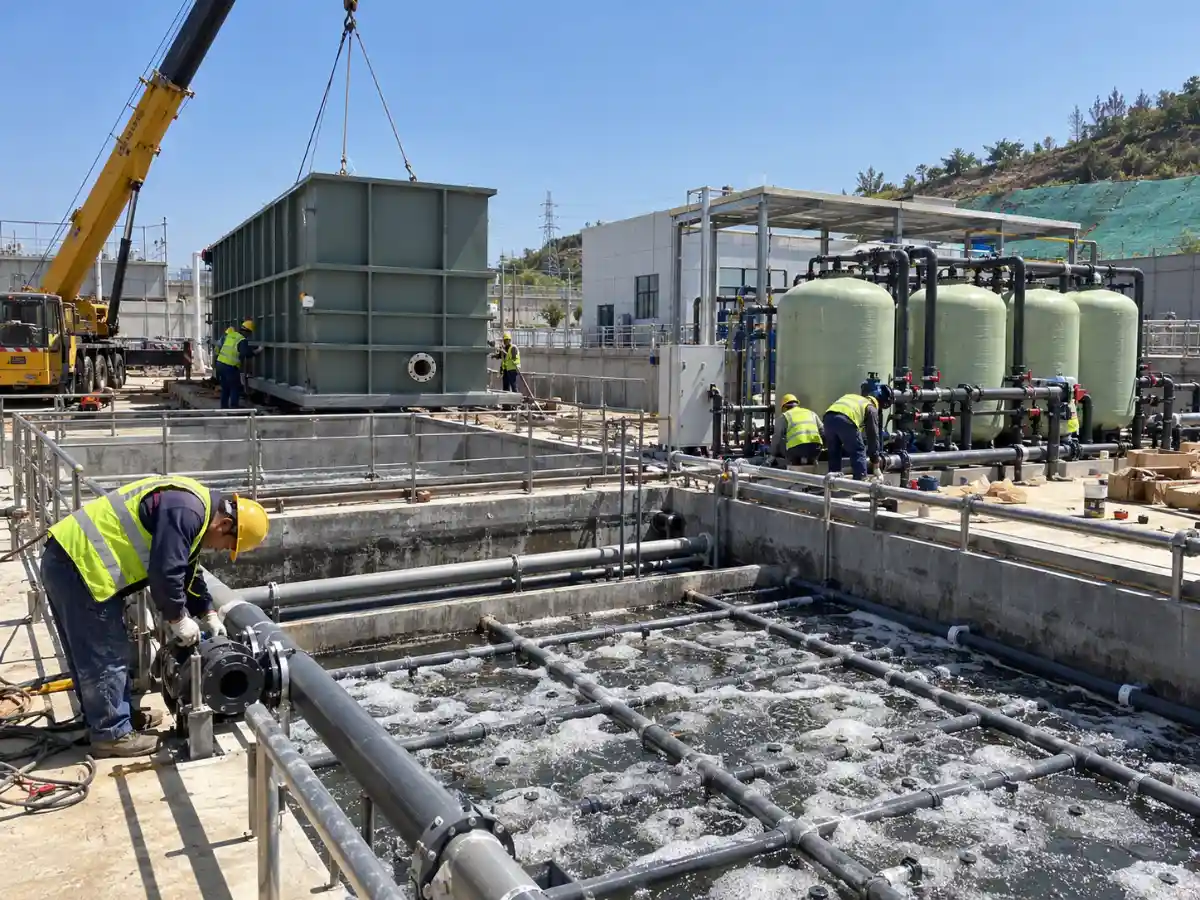
Design Details That Affect Price and Performance
Heat Exchanger Type
Falling film, rising film, and forced circulation are the three main configurations. Falling film gives the best heat transfer per unit area and lowest residence time, which matters for heat-sensitive products. Forced circulation handles scaling and crystallizing streams better but uses more pumping power and costs more.
For most industrial wastewater, falling film with a forced circulation loop on the concentrate side is a good compromise. It keeps the bulk of the evaporation in the efficient falling-film mode while giving you a way to handle the thick stuff at the bottom.
Tube material selection deserves more attention than it usually gets. I’ve seen 316L tubes fail in under 18 months on chloride-containing wastewater. Duplex or titanium would have cost 30% more upfront and lasted a decade.
Vacuum System
You need vacuum to keep the boiling points low enough to use the vapor from one effect to drive the next. Steam ejectors are cheap to buy and simple to operate, but they consume steam — which eats into your steam economy. Liquid ring vacuum pumps cost more upfront and use electricity, but they don’t consume the steam you’re trying to save.
On a triple-effect running 8,000 hours a year, the difference in operating cost between ejectors and liquid ring pumps can be $20,000–$60,000 annually. That usually justifies the higher capital cost of the pumps within 2–4 years.
Controls and Instrumentation
A triple-effect evaporator is a coupled system. Change the feed rate to the first effect and the second and third effects respond. Without good controls, you get oscillation, fouling, and poor steam economy.
At minimum, you want feed flow control, level control on each effect, steam flow control, and concentration control on the product. Temperature and pressure transmitters on each effect are standard. Analyzers for concentration — conductivity or refractive index — are worth the money if your product specification is tight.
I’ve seen plants try to run triple-effect units on manual control. It works, sort of, but the steam consumption is 15–25% higher than it should be and the operators are constantly chasing the system.
Operating Costs: The Numbers That Matter
Capital cost is a one-time hit. Operating cost is forever. Here’s what to expect on a typical triple-effect system:
| Cost Item | Typical Range | Notes |
|---|---|---|
| Steam consumption | 0.38–0.45 kg steam / kg water evaporated | Depends on feed temperature and boiling point elevation |
| Electricity | 15–35 kWh per ton water evaporated | Pumps, vacuum system, controls |
| Cooling water | 20–40 m³ per ton water evaporated | If using surface condenser |
| Antiscalant / chemicals | $0.50–$3.00 per ton water evaporated | Highly dependent on stream chemistry |
| Maintenance labor | $8,000–$25,000 per year | Excludes major overhauls |
Steam is usually the dominant cost. At $20 per ton of steam, you’re looking at $8–9 per ton of water evaporated just for steam. That’s why steam economy matters so much, and why a triple-effect can be worth the extra capital over a double-effect on a large, continuous duty.
But here’s the catch: those numbers assume clean operation. If your heat exchangers foul and you’re cleaning every two weeks, your effective steam consumption goes up, your capacity goes down, and your maintenance costs triple. Pretreatment and antiscalant selection are not optional extras.
Maintenance and Common Failure Points
Triple-effect evaporators are robust machines, but they have predictable failure modes:
- Heat exchanger fouling. The number one issue. Scaling on the tube side reduces heat transfer, which forces you to raise steam pressure or accept lower capacity. Cleaning frequency depends on your stream — I’ve seen everything from monthly to twice a year.
- Vacuum system degradation. Ejector nozzles erode, liquid ring pumps lose clearance, and seals wear. A small vacuum loss raises boiling points across all three effects and quietly costs you money every hour.
- Pump seal failures. Circulation pumps on the concentrate side see high solids and high temperature. Mechanical seals fail. Cartridge seals with flush plans last longer.
- Level control issues. Fouled level instruments cause operators to run effects at the wrong level, which leads to entrainment and product loss.
- Corrosion. Chlorides, low pH, and high temperature are a bad combination for stainless steel. If your stream has chlorides above a few hundred ppm, plan for higher alloys.
The single best thing you can do for maintenance is install a clean-in-place system sized for the job. Manual cleaning of a triple-effect unit takes days. CIP takes hours.
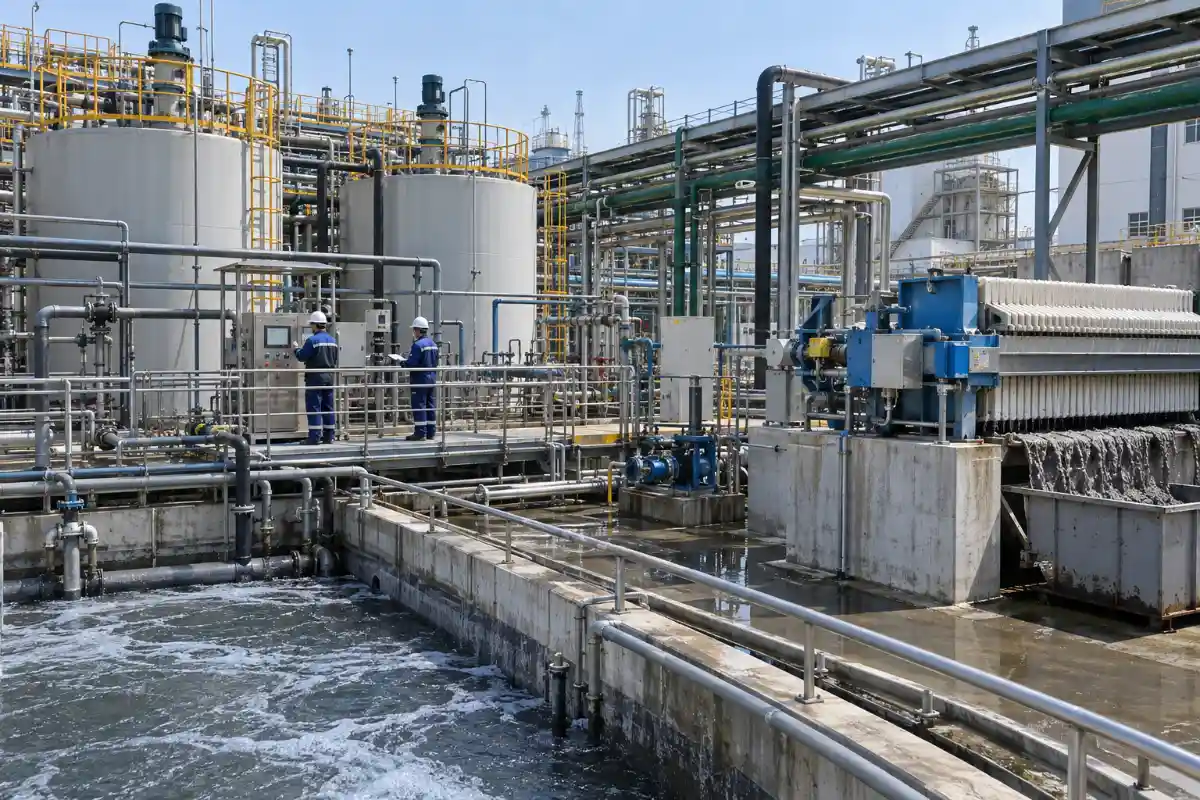
When Triple-Effect Isn’t the Answer
I turn down triple-effect projects when the application doesn’t fit. Here’s when I steer clients elsewhere:
Small flows. Below about 2–3 t/h evaporation, the added complexity of three effects rarely pays back. A single or double-effect unit is simpler to operate and cheaper to maintain.
High fouling streams. If your stream scales aggressively, the third effect will foul and you’ll spend more time cleaning than evaporating. Consider a mechanical vapor recompression system with forced circulation, or pretreat the stream before evaporation.
Heat-sensitive products. The third effect runs cold, but sometimes too cold for the product to stay in solution or for the concentrate to remain pumpable. Check your solubility curve before committing.
Unstable operation. If your feed varies widely in flow or composition, a triple-effect system is hard to control. You may be better off with a more forgiving single-effect or a membrane preconcentration step upstream.
Zero liquid discharge with crystallizer. If you’re going all the way to dry solids, the evaporator is just one part of the system. The crystallizer and solids handling often dominate the cost. Look at the whole zero liquid discharge train before optimizing the evaporator alone.
How to Get an Accurate Quote
Vendors can’t price what they can’t see. If you want a quote that holds up, provide:
- Feed flow rate (minimum, normal, maximum) in m³/h or gpm
- Feed composition — full ionic analysis, TDS, TSS, COD, pH
- Target concentrate concentration and any product specifications
- Available steam pressure, temperature, and cost per ton
- Electrical supply voltage and available power
- Cooling water temperature and availability
- Site conditions — indoor/outdoor, ambient temperature range, seismic zone
- Discharge requirements for the distillate
If you can’t provide a full ionic analysis, at least give total dissolved solids, chlorides, sulfates, and silica. Those four numbers tell a vendor more about materials selection than anything else.
Be honest about turndown requirements. A system designed for 10 t/h but operated at 3 t/h most of the time will not perform the way the datasheet says. Tell the vendor upfront.
Frequently Asked Questions
How much does a triple-effect evaporator cost?
Installed cost typically falls between $180,000 and $1.2 million, with most industrial wastewater systems landing in the $350,000–$800,000 range. The biggest variables are evaporation capacity, heat exchanger materials, and whether the unit ships skid-mounted or field-erected. A 5 t/h system in 316L might be $400,000; a 15 t/h system in duplex with full automation could exceed $1 million.
What’s the difference between a triple-effect and an MVR evaporator?
A triple-effect uses steam to drive evaporation and achieves roughly 2.5 kg of water evaporated per kg of steam. An MVR evaporator uses a mechanical compressor to recompress the vapor and reuse it, achieving the equivalent of 10–25 kg per kg of steam — but it consumes electricity instead. MVR has higher capital cost but much lower operating cost when electricity is reasonably priced relative to steam.
How do I know if a triple-effect evaporator is right for my application?
Start with three numbers: evaporation rate, steam cost, and stream fouling tendency. If you’re evaporating more than 5 t/h, paying more than $12–15 per ton of steam, and your stream doesn’t scale aggressively, a triple-effect is usually a good fit. Below those thresholds, a double-effect or MVR system often makes more sense.
What maintenance does a triple-effect evaporator need?
Expect to clean heat exchangers every 1–12 months depending on your stream. Vacuum system components need inspection annually. Pumps and seals should be checked quarterly. Budget 2–4% of capital cost per year for maintenance, and more if your stream is aggressive. A clean-in-place system pays for itself quickly by cutting downtime.
Can a triple-effect evaporator handle high-chloride wastewater?
Yes, but material selection is critical. Standard 316L stainless will pit and crack under high chloride and temperature. Duplex stainless, super duplex, or titanium are the usual choices. The cost premium is real — 20–60% on wetted parts — but the alternative is replacing heat exchangers every couple of years.
Why is my triple-effect evaporator not reaching design capacity?
The three most common causes are heat exchanger fouling, vacuum loss, and non-condensable gas buildup. Check the vacuum reading on each effect first — a small leak or a degraded ejector will raise boiling points across the whole train. If vacuum is fine, look at the heat exchanger pressure drop; rising pressure drop usually means fouling. Finally, verify that the non-condensable vent is working and that your steam supply is at the pressure and quality the system was designed for.
What’s the typical lead time for a triple-effect evaporator?
For a skid-mounted system, 16–24 weeks is typical. Field-erected systems with custom vessels and site-specific civil work can run 30–40 weeks. Material availability — particularly for titanium and duplex — can add several weeks. If you’re on a tight schedule, get the heat exchanger tubes ordered early.
Final Thoughts
Triple-effect evaporators are a mature, well-understood technology. The engineering isn’t the hard part — the hard part is matching the system to your actual stream, your actual steam cost, and your actual operating reality. Get those three things right and the capital cost is a detail. Get them wrong and no amount of clever design will save you.
If you’re in the early stages of evaluating options, the most useful thing you can do is gather good data on your feed stream and be honest about how the plant will actually operate. Everything else follows from there.
Need help sizing a triple-effect evaporator for your wastewater stream? Share your feed data and we’ll walk through the design options with you.