

If you’re specifying equipment for pharmaceutical wastewater, the honest answer is that no single machine handles the whole job. The right approach combines pretreatment, biological treatment, and a final barrier — usually membrane or evaporation — chosen around your actual stream chemistry. In my experience, most failures trace back to one mistake: treating pharma effluent like municipal sewage. It isn’t. It swings in strength, carries solvents and antibiotics, and varies batch to batch. The best wastewater treatment equipment for pharmaceutical industry applications is the set of units matched to those realities, not a catalog list.
Below I’ll walk through how I think about each stage, where the costs hide, and what actually holds up in the field.
Why Pharmaceutical Wastewater Breaks Standard Designs
Pharma plants rarely produce one steady stream. You get high-COD process water from fermentation or synthesis, cleaning-in-place (CIP) caustics, spent solvents, and low-strength rinse water — often all in the same day. The variability alone defeats fixed-parameter designs.
Three characteristics drive equipment selection:
- High organic load and toxicity. COD can run from a few hundred to tens of thousands of mg/L depending on the product. Some compounds inhibit biological treatment at low concentrations.
- Salinity and refractory organics. Salt-rich streams from API production resist conventional biology and corrode carbon steel.
- Batch behavior. Campaign manufacturing means flow and load change weekly. Equipment must tolerate turndown without losing efficiency.
If you design for average conditions, you’ll fail on peak days. Design for the peak and control the average.
Stage 1: Pretreatment and Equalization
Everything downstream depends on this stage. I’ve seen excellent membrane systems fouled within months because equalization was undersized.
Equalization and buffering
Size equalization for at least one full production cycle, not just daily flow. For campaign plants, that may mean 24–72 hours of hydraulic retention. Add mixing and, where solvents are present, consider covered tanks with vapor handling.
Chemical and physical pretreatment
- pH adjustment and neutralization — essential before biology or membranes.
- Coagulation and flocculation — removes suspended solids and some colloidal COD.
- Dissolved air flotation (DAF) — effective where oils, fats, or floatable solids appear.
- Advanced oxidation (Fenton, ozone, UV/H₂O₂) — breaks refractory compounds before biology. Use selectively; chemical cost adds up fast.
Pretreatment isn’t glamorous, but it protects the expensive equipment behind it. Skipping it is the most common cost-saving mistake I see.
Stage 2: Biological Treatment
Biology handles the bulk of biodegradable COD at the lowest operating cost. The question is which configuration.
Options and trade-offs
| Technology | Best for | Main limitation |
|---|---|---|
| Conventional activated sludge | Moderate COD, stable flow | Poor tolerance to toxicity and load swings |
| MBBR (moving bed biofilm) | Load variability, retrofit | Media management, aeration demand |
| MBR (membrane bioreactor) | High-quality effluent, small footprint | Membrane fouling, higher energy |
| Anaerobic (UASB/EGSB) | High-strength streams, energy recovery | Sensitive to toxicity, slow startup |
For high-strength streams, anaerobic pretreatment cuts aeration energy dramatically and produces biogas. But it’s fragile — a toxic batch can kill the biomass for weeks. I usually recommend it only where the stream is consistent and the operator has real process control capability.
For most pharma sites, MBR gives the best balance: consistent effluent quality that protects the downstream barrier, in a footprint that fits inside existing buildings. The trade-off is membrane replacement cost and the discipline to keep fouling under control.
Stage 3: The Final Barrier — Membranes and Evaporation
After biology, you still have dissolved salts, residual organics, and sometimes trace active compounds. This is where the choice gets expensive, so it deserves the most engineering attention.
Membrane separation
Reverse osmosis concentrates dissolved solids and produces clean permeate. Standard RO works when salinity is moderate and fouling is controlled. For high-salinity or high-fouling streams, disc-tube RO (DTRO) handles conditions that would destroy spiral-wound elements.
I’ve used DTRO membrane systems on pharma and leachate projects where conventional RO fouled within weeks. The open-channel design tolerates suspended solids and scaling far better, at the cost of higher pressure and energy.
For high-pressure duty, high-pressure RO pushes recovery higher but demands careful pretreatment and scaling control. Above certain concentration limits, membrane alone stops being economical — that’s when evaporation takes over.
Evaporation and concentration
Thermal evaporation handles the streams membranes can’t: very high salinity, high COD, or where you need near-total volume reduction. The core choice is between multi-effect and mechanical vapor recompression.
- Multi-effect evaporators reuse steam across stages. Steam-driven, so operating cost tracks your steam price. Good where cheap steam is available.
- MVC/MVR evaporators use a compressor to recompress vapor and reuse its heat. Electric-driven, so cost tracks electricity. Usually the lower-opex choice where power is reasonably priced.
For a detailed look at how heat exchangers drive evaporator performance and fouling behavior, that’s often where the real design risk sits.
Where discharge is restricted or zero liquid discharge is required, an integrated ZLD system combines membrane concentration with evaporation and crystallization. It’s capital-heavy and energy-intensive, so it only makes sense where regulations or water reuse justify it.
Sludge dewatering
Biological treatment generates sludge, and how you dewater it affects disposal cost more than most people expect. A screw press gives continuous, low-attention operation with decent dry solids. Centrifuges reach higher dryness but consume more power and need more maintenance. The right choice depends on your disposal route and labor model.
Equipment Selection Logic: How I Actually Decide
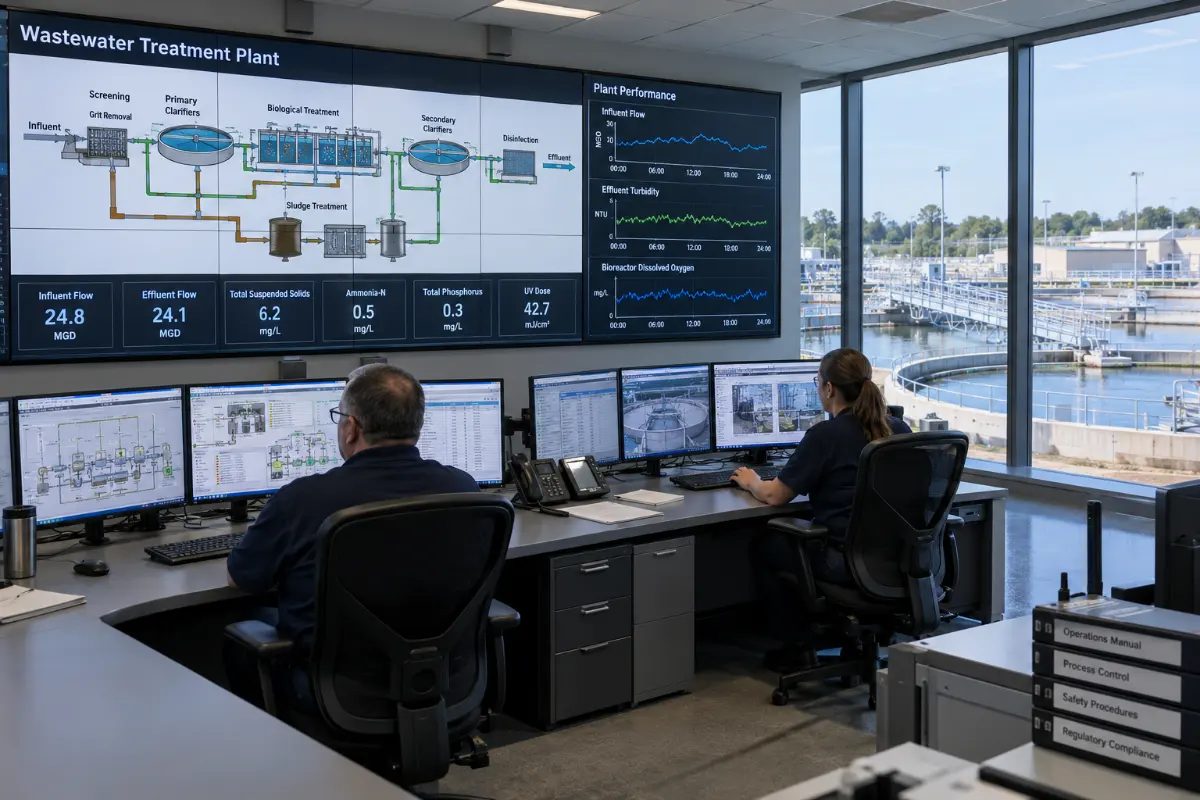
When I sit down with a client’s water analysis, I work through a sequence rather than jumping to a technology.
- Characterize the stream. COD, BOD, TDS, salinity, pH, toxicity, temperature, and variability — not just averages.
- Confirm the discharge or reuse target. This sets how many treatment stages you actually need.
- Match the barrier to the water. Moderate salinity → RO. High salinity or fouling → DTRO or evaporation. Near-zero discharge → ZLD.
- Check the energy source. Steam available and cheap → multi-effect. Power cheap → MVC.
- Model lifecycle cost, not just capex. Energy, chemicals, membranes, and labor usually dominate over 10 years.
One thing I tell every client: the cheapest system to buy is rarely the cheapest to run. A slightly higher capital cost that cuts energy or membrane replacement often pays back within a few years.
Energy and Lifecycle Cost: Where the Money Goes
Pharma wastewater treatment is energy- and chemical-intensive. Typical cost drivers, in rough order of impact:
- Aeration — the biggest electrical load in biological treatment. Fine-bubble diffusers and dissolved-oxygen control matter.
- Evaporation — either steam or compressor power, depending on technology. This is often the single largest operating line for high-salinity sites.
- Membrane replacement — a recurring cost that surprises people who only budgeted capex.
- Chemicals — pH adjustment, antiscalant, cleaning agents, and oxidation chemicals.
- Sludge disposal — highly variable by region and regulated as hazardous in many cases.
Indicative ranges are useful for early budgeting but should always be confirmed with a water analysis. Published figures vary widely because feed chemistry drives everything.
Design tip: model your operating cost at three feed concentrations — low, average, and peak. If the system isn’t economic at peak, it isn’t economic.
Maintenance and Common Failure Points
Most problems I get called in to fix fall into a few predictable categories.
Membrane fouling and scaling
Usually caused by inadequate pretreatment, wrong antiscalant, or recovery set too high. Fix the pretreatment before blaming the membrane.
Evaporator scaling and fouling
Heat exchanger surfaces foul, especially with high hardness or organics. Cleaning frequency and chemical selection determine whether the unit runs reliably. Forced-circulation designs tolerate scaling better than falling-film in dirty service.
Biological upset
Toxic shock from a batch discharge, or nutrient imbalance. Equalization and toxicity monitoring prevent most of these. Once biomass is damaged, recovery takes weeks.
Instrumentation drift
pH, conductivity, and DO probes drift. Calibration discipline is unglamorous but prevents more failures than any equipment upgrade.
If you’re evaluating a system and want a second opinion on the design logic, that’s a conversation worth having early rather than after commissioning.
Putting It Together: A Realistic System Layout
For a typical API or formulation plant with mixed streams, a workable configuration looks like this:
- Segregation of high-strength and low-strength streams
- Equalization with mixing and pH control
- Chemical pretreatment (coagulation/flocculation, DAF where needed)
- Anaerobic pretreatment for the highest-strength stream (if consistent)
- Aerobic MBR for polishing
- RO or DTRO for dissolved solids removal
- Evaporation or ZLD for concentrate management
- Screw press or centrifuge for sludge dewatering
Not every plant needs all eight. But the logic — protect the expensive units with good pretreatment, match the barrier to the water, and control variability — holds everywhere.
If you want to talk through your specific stream and constraints, you can reach our engineering team here. We’d rather help you get the design right than sell you equipment you don’t need.
Frequently Asked Questions
What’s the single most important factor in choosing pharmaceutical wastewater equipment?
Accurate stream characterization. COD, salinity, toxicity, and variability drive every downstream decision. Without reliable data, any equipment choice is a guess.
Should I use membranes or evaporation for high-salinity pharma wastewater?
Start with membranes if salinity is moderate and fouling is manageable. Move to evaporation when concentration limits, scaling, or zero-discharge requirements make membrane recovery uneconomical. Many systems combine both.
How much does a pharmaceutical wastewater treatment system cost?
Capital cost depends heavily on flow, load, and the required barrier technology. Operating cost is usually dominated by energy, membranes, chemicals, and sludge disposal. Get a water analysis first — budgets built on assumptions are unreliable.
How often do membranes need replacement?
It varies with feed quality and cleaning discipline. Well-maintained RO elements can last several years; severe fouling shortens that significantly. Pretreatment quality is the biggest lever.
Why does biological treatment fail so often in pharma plants?
Usually toxicity shock or load variability, not the biology itself. Equalization, stream segregation, and toxicity monitoring prevent most upsets.
Is anaerobic treatment worth it for high-strength streams?
Yes, where the stream is consistent and you have process control capability. It cuts aeration energy and produces biogas. But it’s sensitive to toxic batches, so it needs careful operation.
What maintenance matters most?
Instrument calibration and cleaning schedules. pH, conductivity, and DO probes drift, and fouled heat exchangers or membranes degrade efficiency quietly. Preventive maintenance beats emergency repair every time.