

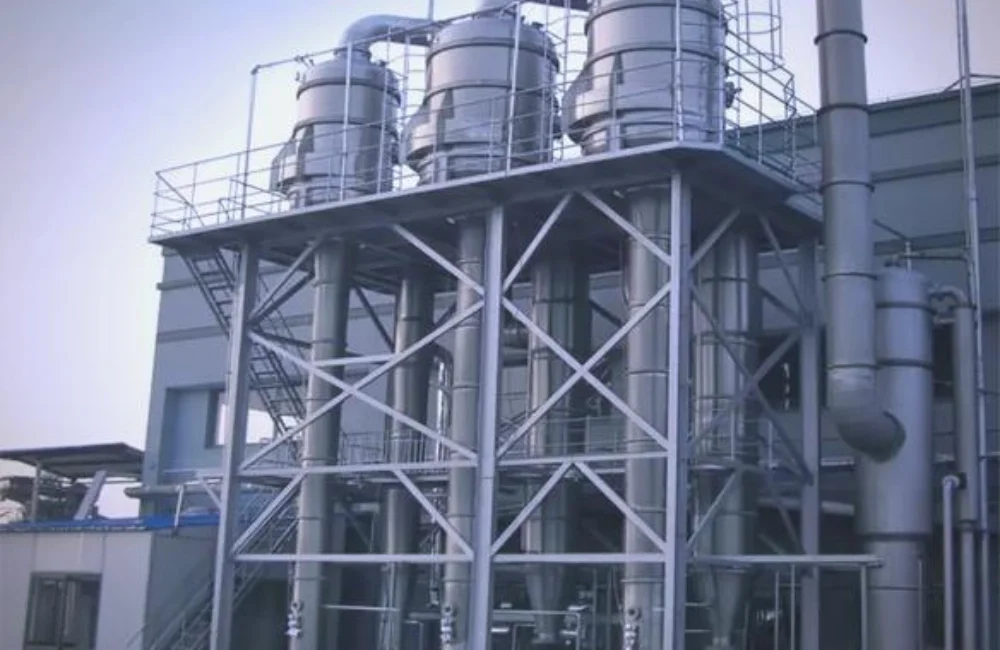
An MVR evaporator, short for Mechanical Vapor Recompression evaporator, reuses the vapor produced during evaporation as a heating source. The vapor is compressed to raise its pressure and saturation temperature, then returned to the evaporator heat exchanger where it condenses and supplies heat for further evaporation.
Compared with a conventional steam-heated evaporator, this arrangement can substantially reduce the amount of live steam required during normal operation. For this reason, MVR evaporation is widely considered for industrial wastewater concentration, brine treatment, product concentration and some Zero Liquid Discharge (ZLD) systems.
In industrial evaporation projects, the terms MVR and MVC (Mechanical Vapor Compression) are sometimes used for similar compressor-driven vapor reuse systems. Memva uses both terms across different equipment and project documents. In this article, we use MVR evaporator for consistency.
How an MVR Evaporator Works
The basic idea behind an MVR evaporator is straightforward: instead of allowing the energy in the generated vapor to leave the process through a condenser, the system recovers most of that vapor and raises its pressure with a mechanical compressor.
Increasing the vapor pressure also increases its saturation temperature. Once the compressed vapor is hotter than the liquid being evaporated, it can be used on the heating side of the heat exchanger. The vapor then condenses and releases latent heat, which drives further evaporation.
A typical MVR evaporation process includes the following steps:
1. Feed Preheating
The feed is normally preheated before it enters the main evaporation section. Heat from condensate, concentrate or other available process streams can be recovered for this purpose. Good heat integration reduces the amount of energy required to bring the feed to its operating temperature.
2. Evaporation and Vapor Separation
The heated liquid enters the evaporator, where part of the water is converted to vapor. A separator removes entrained liquid droplets from the vapor before it reaches the compressor.
This separation step is important. Liquid carryover can affect compressor operation, while excessive entrainment may also reduce distillate quality.
3. Vapor Compression
The secondary vapor enters a mechanical compressor. Depending on the required flow rate and pressure increase, an MVR system may use a centrifugal compressor, Roots-type compressor or another compressor configuration.
The compressor supplies mechanical energy to the vapor, increasing its pressure and temperature. The required pressure rise depends largely on the temperature difference needed for heat transfer and the boiling point elevation (BPE) of the process liquid.
4. Heat Recovery and Condensation
The compressed vapor returns to the heating side of the evaporator. As it condenses, its latent heat passes through the heat-transfer surface and evaporates more water from the process liquid.
The resulting condensate can sometimes be reused as process water, but its actual quality depends on the feed composition, vapor-liquid separation efficiency and the presence of volatile compounds. It should not automatically be treated as clean water without analysis.
5. Concentrate Recirculation and Discharge
As evaporation continues, dissolved salts and other non-volatile components become more concentrated. Depending on the process, part of the concentrate may be circulated through the heat exchanger to maintain liquid velocity and control heat transfer.
Once the target concentration is reached, concentrate is removed for further treatment, crystallization, recovery or disposal.
For wastewater with significant scaling tendency or solids formation, a forced-circulation evaporator may be more appropriate than a falling-film design. The evaporator configuration should therefore be selected from the actual feed characteristics rather than from evaporation capacity alone.
You can also review Memva’s MVC/MVR evaporator systems for equipment configurations used in industrial wastewater applications.
What Determines MVR Energy Consumption?
There is no single electricity-consumption figure that applies to every MVR evaporator. Power demand depends on the amount of vapor being compressed and, more importantly, how much pressure and temperature lift the compressor must provide.
The main factors include:
- Boiling point elevation: Concentrated salt solutions boil at a higher temperature than pure water at the same pressure. A higher BPE generally requires a larger compressor temperature lift and increases power demand.
- Feed concentration and final concentration: As concentration increases, BPE, viscosity and scaling tendency may also increase.
- Heat-transfer temperature difference: A larger temperature difference can reduce the required heat-transfer area, but usually requires more vapor compression.
- Compressor efficiency: Compressor selection and operating point have a direct effect on specific electricity consumption.
- Heat exchanger condition: Scaling and fouling increase thermal resistance. As heat transfer deteriorates, operating performance can decline.
- Feed temperature and heat recovery: Preheating the feed with available condensate or process heat reduces the thermal load.
- Non-condensable gases and vapor quality: Poor vapor separation or accumulation of non-condensable gases can interfere with heat transfer and stable operation.
This is also why a statement such as “an MVR evaporator always uses 30–50 kWh per ton of water” should be treated as a rough reference rather than a design specification.
For example, a U.S. EPA / ENERGY STAR industry guide cites approximately 41 kWh of electricity per ton of water evaporated for an MVR application in chlor-alkali processing.[1] This is a useful reference point, but it describes a particular industrial application rather than all MVR systems.
Research on concentrated sodium chloride solutions has also shown that increasing solution concentration and boiling point elevation can significantly increase compressor power demand.[3]
For an actual wastewater project, electricity consumption should therefore be estimated from the feed analysis, evaporation load, operating temperature, BPE, compressor performance and required final concentration.
MVR vs. Traditional Evaporation
The main difference between MVR and conventional evaporation is how the vapor energy is reused.
A single-effect evaporator normally uses live steam as its primary heat source. A multi-effect evaporator improves steam economy by using vapor from one effect to heat the next effect at a lower pressure.
An MVR evaporator takes a different approach. It mechanically recompresses the generated vapor so that it can be reused at a higher temperature in the evaporation process.
| Item | MVR Evaporator | Multi-Effect Evaporator | Single-Effect Evaporator |
|---|---|---|---|
| Primary purchased energy | Mostly electricity for vapor compression | Steam plus electricity for pumps and auxiliaries | Primarily steam plus auxiliary electricity |
| How vapor heat is reused | Vapor is mechanically compressed and returned as heating vapor | Vapor from one effect heats the next effect | Limited vapor heat recovery in a basic system |
| Continuous live-steam demand | Usually much lower; actual requirement depends on heat balance and operating conditions | Required for the first effect | Required continuously |
| Cooling requirement | Usually lower, although cooling or condensation may still be required for excess vapor and auxiliaries | A condenser is normally required for final vapor | A condenser is normally required when vapor is not otherwise recovered |
| Main equipment consideration | Compressor, heat exchanger and vapor separation | Multiple effects, vacuum system and steam distribution | Simple equipment arrangement |
| Often considered when | Continuous evaporation load is significant and steam cost is high | Steam or waste heat is readily available | Capacity is small or low initial investment is the priority |
| Important limitation | Performance is sensitive to required temperature lift, BPE, fouling and compressor operating range | More effects increase equipment size and complexity | Higher steam consumption per unit of water evaporated |
MVR is therefore not automatically the lowest-cost solution for every plant. A facility with inexpensive waste steam may reach a different conclusion from a facility that purchases steam at a high cost but has reliable electrical power.
Annual operating hours also matter. Because an MVR system includes a vapor compressor and associated controls, the capital cost can be higher than that of a simple steam-heated evaporator. Whether that additional investment makes economic sense should be evaluated against local electricity prices, steam costs, evaporation capacity, annual operating hours and maintenance requirements.
A fixed claim such as “12-month payback” is rarely useful without those project inputs. A proper comparison should use the site’s actual utility costs and operating conditions.
Applications in Industrial Wastewater Treatment
MVR evaporators are used in wastewater treatment when a dissolved or suspended load must be concentrated and membrane or biological treatment alone cannot achieve the required volume reduction.
The suitability of MVR still depends on the wastewater chemistry. Salts, hardness, silica, organics, ammonia, suspended solids, oil, foaming tendency and corrosive ions can all influence the process design.
Landfill Leachate Treatment
Landfill leachate can contain high concentrations of dissolved salts, ammonia, refractory organic matter and other contaminants. Its composition can also vary substantially with landfill age, climate and upstream treatment.
An MVR evaporator can be used to reduce the volume of a concentrated leachate stream, particularly after biological or membrane treatment. The non-volatile dissolved material remains mainly in the concentrate while water is evaporated and recovered as condensate.
However, some ammonia and volatile organic compounds may transfer into the vapor phase. Condensate quality therefore needs to be checked, and additional treatment may be required before discharge or reuse.
See Memva’s landfill leachate treatment project for an example of how evaporation can be combined with other treatment stages.
Electroplating and Metal Finishing
Electroplating wastewater may contain nickel, chromium, zinc, copper and other dissolved metals together with acids, alkalis and salts.
Because most metal salts are non-volatile, evaporation can concentrate them into a much smaller liquid volume while recovering part of the water as condensate. Depending on the chemistry, the concentrate may then be sent for recovery, crystallization or controlled disposal.
In rinse-water applications, recovered condensate may also be suitable for reuse after confirming that it meets the required water-quality specification.
High chloride levels and aggressive process chemistry require careful material selection. The correct metallurgy cannot be selected from TDS alone; the complete ion composition, pH, temperature and expected concentration factor need to be considered.
More information is available in Memva’s electroplating wastewater treatment case.
Pharmaceutical Wastewater
Pharmaceutical wastewater can contain salts, APIs, intermediates and organic compounds that make conventional biological treatment difficult.
Evaporation can be useful when the objective is to reduce the volume of a high-strength stream or separate water from non-volatile dissolved material. Operation under vacuum can also allow evaporation at a lower boiling temperature.
One important limitation is volatility. Organic solvents, ammonia and other volatile compounds may enter the vapor and condensate rather than remaining completely in the concentrate. For this reason, pharmaceutical wastewater should be evaluated for vapor composition, safety requirements and downstream condensate treatment before an MVR process is selected.
See Memva’s pharmaceutical wastewater treatment project for additional application context.
The Role of MVR in Zero Liquid Discharge (ZLD)
MVR evaporation is commonly used as a thermal concentration step in Zero Liquid Discharge systems, but it is only one part of the overall process.
A typical industrial ZLD arrangement may include:
- Pretreatment: Removal or control of hardness, suspended solids, oil, silica or other components that could interfere with downstream equipment.
- Membrane concentration: Reverse osmosis, nanofiltration or a high-pressure membrane process such as DTRO may be used when the water chemistry allows it.
- Thermal concentration: The remaining brine is fed to an MVR or another evaporator to remove additional water.
- Crystallization or final solids handling: When solid salts need to be produced, a crystallizer and solid-liquid separation equipment may follow the concentration stage.
Using membranes before evaporation can be economically attractive because membrane separation generally requires less energy than evaporating the same amount of water thermally. The optimum recovery point, however, depends on osmotic pressure, scaling risk and wastewater composition.
An MVR evaporator is therefore often positioned after the practical membrane recovery limit rather than used to treat the full wastewater flow from the beginning.
For streams approaching salt saturation, forced circulation, crystallization control and solids handling become increasingly important. A standard falling-film MVR evaporator should not automatically be assumed to perform the same duty as an evaporation crystallizer.
It is also worth defining what ZLD means for the specific plant. The liquid stream may be eliminated within the treatment boundary, but concentrated salts, sludge or mixed solids still require recovery, reuse or disposal.
Memva provides integrated ZLD system design combining membrane, evaporation and solids-management processes according to the wastewater characteristics.
What to Check Before Selecting an MVR Evaporator
The compressor is an important part of an MVR system, but compressor selection alone does not determine whether the evaporator will operate well.
The starting point should be the feed chemistry and the required process result.
Feed Analysis
A useful water analysis normally includes the major dissolved ions, TDS, COD or TOC, pH, suspended solids, hardness, silica and other contaminants relevant to the particular wastewater.
When the solution will be concentrated several times, it is also necessary to consider what happens at the final concentration, not just the composition of the incoming feed.
Salts that are fully dissolved at the inlet may begin to precipitate as water is removed.
Boiling Point Elevation
BPE is one of the most important inputs for an MVR design. A high BPE reduces the effective temperature driving force available for heat transfer and may require a greater compressor pressure rise.
For difficult high-concentration solutions, laboratory testing or measured boiling-point data can be more useful than estimating performance from TDS alone.
Falling Film or Forced Circulation
Falling-film evaporators provide efficient heat transfer and short residence time for suitable clean or moderately fouling feeds.
Forced-circulation systems use higher liquid circulation velocities and are often considered when the stream has greater scaling potential, higher viscosity or suspended/crystallizing solids.
The choice should be based on the behavior of the process liquid as it becomes concentrated.
Material Selection
Stainless steel is not automatically suitable for every industrial wastewater.
Chloride concentration, pH, temperature and oxidizing conditions can substantially affect corrosion risk. Depending on the wastewater, materials may include 316L stainless steel, duplex stainless steel, titanium or other corrosion-resistant alloys.
Material selection should be based on the actual operating environment and expected concentrate composition rather than a general rule such as “high TDS requires duplex steel.”
Compressor Selection
The compressor must match the vapor flow, suction condition, required pressure ratio and operating range of the evaporator.
It is also important to consider liquid carryover protection, vibration monitoring, control range, maintenance access and the expected variation in evaporation load.
Mechanical vapor recompression systems generally work best when the compressor and evaporator are designed as one process system rather than selected independently.
Cleaning and Fouling Control
An evaporator that performs well when clean may consume more energy after scale builds on the heat-transfer surface.
The design should therefore consider:
- Expected scaling compounds
- Required circulation velocity
- CIP chemistry
- Cleaning frequency
- Access for inspection
- How cleaning affects plant operating time
For difficult wastewater, pilot testing can help determine scaling behavior and cleaning requirements before the full-scale system is finalized.
Controls and Operating Range
An industrial MVR system typically uses PLC-based controls to coordinate feed flow, liquid level, vacuum, temperature, compressor operation and concentrate discharge.
Automation is important, but it does not remove the need for a stable process design. If feed composition or flow varies substantially, those variations should be defined during the design stage so the control system and equipment can accommodate them.
Performance Conditions
Equipment performance should be discussed together with clearly defined feed and utility conditions.
For example, an evaporation-capacity or energy-consumption target only has meaning when the following are specified:
- Feed flow and composition
- Feed temperature
- Required final concentration
- Evaporation temperature and pressure
- Boiling point elevation
- Available electricity and startup steam
- Expected operating hours
- Allowable fouling or cleaning interval
This is more useful than a general performance guarantee that does not define the operating envelope.
Information Needed for Preliminary MVR Sizing
If you are comparing an MVR evaporator for an existing wastewater stream, the following information is normally enough to begin a preliminary process review:
| Information | Why It Matters |
|---|---|
| Feed flow, m³/h or t/day | Determines evaporation capacity and equipment size |
| TDS and major ion analysis | Used to evaluate concentration, scaling, BPE and material selection |
| COD/TOC and volatile compounds | Helps evaluate fouling and possible transfer into the condensate |
| pH, hardness and silica | Important for scaling and corrosion assessment |
| Suspended solids and oil | Affects pretreatment and evaporator configuration |
| Required final concentration | Determines the concentration factor and final process conditions |
| Annual operating hours | Important for operating-cost and payback calculations |
| Electricity and steam cost | Needed to compare MVR with steam or multi-effect evaporation |
| Existing pretreatment | Shows which contaminants are already controlled upstream |
Memva can use this information to prepare a preliminary process configuration before moving to detailed heat-balance calculations or pilot testing.
If you have a wastewater analysis and design flow available, send the data to Memva for an initial MVR evaporation review.
Frequently Asked Questions About MVR Evaporators
What is the main disadvantage of an MVR evaporator?
The main trade-off is the combination of higher equipment complexity and compressor capital cost compared with a basic steam-heated evaporator. MVR performance also depends on keeping the required vapor temperature lift within a practical range.
High boiling point elevation, severe fouling, large variations in feed conditions or unsuitable compressor operating conditions can reduce the expected energy advantage.
For this reason, MVR should be evaluated on total lifecycle cost rather than equipment price alone.
Can an MVR evaporator handle solids?
Yes, but the evaporator must be designed for the solids load.
A forced-circulation evaporator or crystallizer can keep suspended or crystallizing solids moving through the system and reduce uncontrolled deposition on heat-transfer surfaces. A falling-film evaporator is generally less suitable once significant solids begin forming inside the evaporation circuit.
The expected saturation point and crystal behavior should therefore be considered during process design.
How much electricity does an MVR evaporator use?
There is no universal kWh-per-ton value for an MVR evaporator.
Specific electricity consumption depends on compressor efficiency, evaporation pressure, required temperature lift, boiling point elevation, solution concentration, heat recovery and heat-exchanger condition.
As one published reference, a U.S. EPA / ENERGY STAR guide reports approximately 41 kWh per ton of water evaporated for an MVR application in chlor-alkali processing.[1] Other applications can operate above or below that value.
The correct figure for a project should come from a heat and mass balance based on the actual feed.
Does an MVR evaporator require steam?
External steam is commonly used during startup to bring the system to operating temperature. Once stable evaporation and vapor recompression are established, continuous live-steam demand can be much lower than in a conventional steam-heated evaporator.
However, saying that every MVR system requires “zero steam” during operation is too broad. Depending on process conditions and heat balance, a small amount of additional heat or removal of excess vapor may still be required.[2]
Is MVR suitable for all types of wastewater?
No. MVR is most attractive when there is a meaningful continuous evaporation load and the feed can be concentrated within a practical temperature lift and fouling-control strategy.
High TDS alone does not mean that MVR is automatically suitable. Very high BPE, severe scaling, high viscosity, foaming, volatile contaminants or highly variable feed conditions can change the process design and economics.
For dilute wastewater, membrane treatment may remove water more economically before thermal evaporation is considered.
Is high boiling point elevation good for MVR?
No. High boiling point elevation is generally a design challenge rather than an advantage.
As BPE increases, the vapor compressor usually needs to provide a larger temperature lift before the compressed vapor can transfer heat back to the boiling liquid. This can increase power consumption and may require a different compressor or evaporation configuration.
High-BPE streams can still be treated, but they need to be evaluated specifically rather than treated as a standard MVR duty.
What is the difference between MVR and MVC?
MVR stands for Mechanical Vapor Recompression and describes the process of compressing generated vapor so its heat can be reused.
MVC stands for Mechanical Vapor Compression. In industrial evaporation equipment, suppliers sometimes use MVC and MVR interchangeably when referring to a mechanically compressed vapor-reuse system.
When comparing equipment, the process configuration, compressor duty, evaporator type and guaranteed operating conditions are more important than whether the supplier uses the term MVR or MVC.
What information is needed to size an MVR evaporator?
At minimum, the supplier should know the feed flow, feed temperature, water analysis, TDS, major ions, COD or TOC, pH, suspended solids and required final concentration.
For a more accurate energy estimate, boiling point elevation, available utilities, annual operating hours and local electricity and steam costs should also be provided.
When Does an MVR Evaporator Make Sense?
An MVR evaporator is worth evaluating when a plant has a significant and relatively continuous evaporation duty, wants to reduce dependence on live steam, and has a reliable electrical supply.
It is particularly useful where wastewater must be concentrated beyond the practical recovery limit of membrane treatment, or where recovered condensate and reduced waste volume provide additional value.
It is not automatically the best option for every evaporation project. High BPE, difficult scaling behavior, intermittent production, low annual operating hours or access to inexpensive waste steam can change the economics.
The most reliable way to compare MVR with a multi-effect or conventional evaporator is to use the actual feed chemistry and plant utility costs rather than a generic energy-saving percentage.
If you are currently evaluating an MVR evaporator for industrial wastewater or ZLD, Memva can review your water analysis, flow rate and target concentration and suggest an initial process configuration.
Contact Memva with your wastewater data or review our MVR/MVC evaporator equipment for more information.
References
- U.S. EPA / ENERGY STAR. Energy Efficiency Improvement and Cost Saving Opportunities for the Chlor-Alkali Industry, 2025. The guide discusses mechanical vapor recompression and cites electricity use of approximately 41 kWh per ton of water evaporated for the referenced chlor-alkali application.
- GEA. GEA meVap® Evaporation — Mechanical Vapor Recompression Solutions in Evaporation Processes. Used as a technical reference for vapor recompression, condensate heat recovery and heat-balance considerations in MVR operation.
- Applied Thermal Engineering. Numerical Analysis on the Performance of Mechanical Vapor Recompression System for Strong Sodium Chloride Solution Enrichment. The study examines the effect of solution concentration and boiling point elevation on compressor power and MVR performance.
Published energy values are application-specific and should not be used as guaranteed equipment performance without a project-specific heat and mass balance.