

A 50 KLD zero liquid discharge (ZLD) plant typically lands between $180,000 and $420,000 in capital cost, depending on the wastewater chemistry, the evaporation technology selected, and how much of the system is containerized. The equipment list itself is fairly predictable: pretreatment, membrane concentration, evaporation and crystallization, plus a solids handling train. What changes the number is not the flow rate. It is what is dissolved in the water. I have quoted enough of these systems to know that two projects with identical daily volumes can differ by a factor of two in price, and the reason is almost always the salt load, the organics, and the scaling tendency. This article walks through the equipment list, the cost breakdown, and the engineering decisions that actually move the budget.

What a 50 KLD ZLD Plant Actually Has to Do
Fifty cubic meters per day sounds small. On paper it is roughly 2.1 m³ per hour, which is a modest flow any membrane skid can handle. The problem is never the water volume. It is the salt.
If your feed is 3% total dissolved solids (TDS), you are looking at about 1.5 tons of salt per day that has to leave the site as a solid or a concentrated brine. If the feed is 8% TDS, that number jumps to roughly 4 tons per day. Evaporating water is straightforward engineering. Crystallizing salt and keeping the evaporator from fouling is where the money goes.
A properly designed 50 KLD ZLD train usually has four stages working in sequence:
- Pretreatment — removes suspended solids, hardness, silica, and organics that would foul downstream equipment.
- Membrane concentration — reverse osmosis or DTRO to squeeze as much water out as possible before thermal treatment.
- Evaporation — MVC or MVR to boil off the remaining water at low energy cost.
- Crystallization and solids handling — turns the final brine into a manageable solid, often with a screw press or centrifuge.
Each stage protects the next one. Skip a stage and you pay for it later in cleaning downtime, membrane replacements, or heat exchanger descaling.
The Equipment List, Stage by Stage

1. Pretreatment and Equalization
Every ZLD plant I have commissioned started with a feed tank and some form of chemical conditioning. For a 50 KLD system, the typical pretreatment package includes:
- Equalization tank, 20–40 m³, with mixer and level control
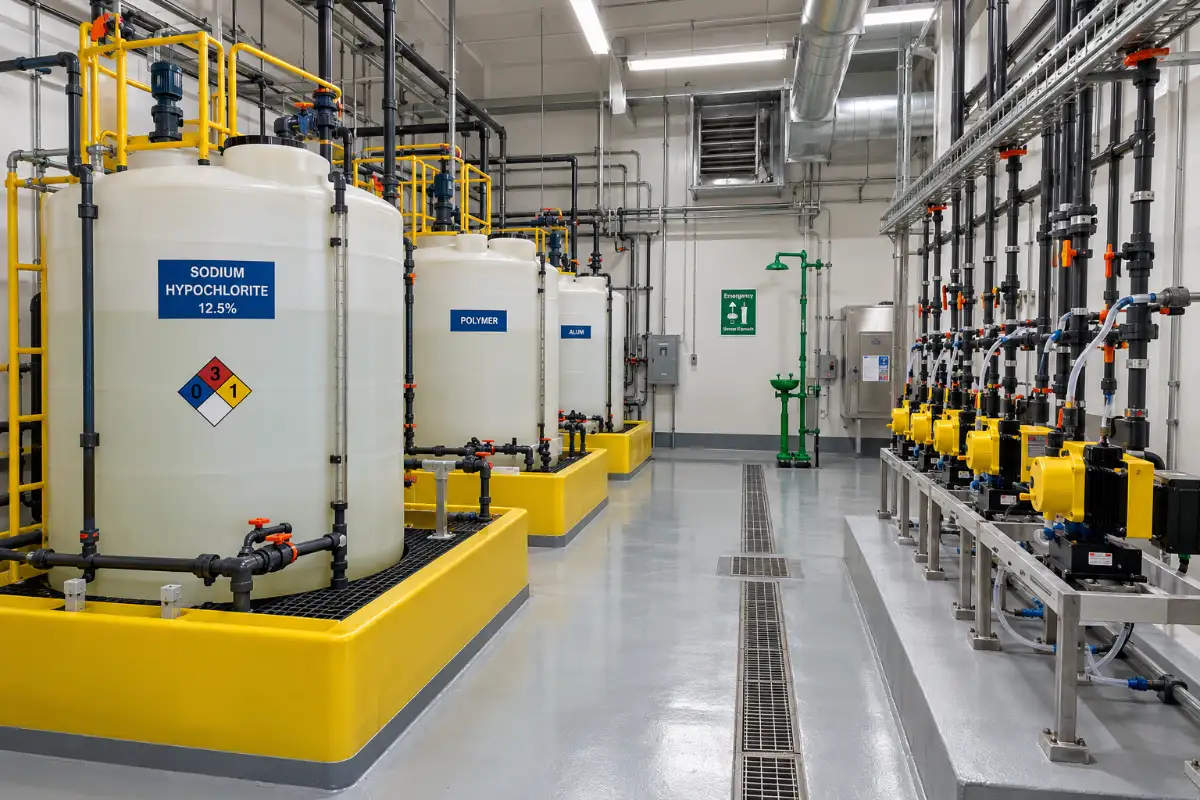
- Chemical dosing skids — acid, caustic, antiscalant, and sometimes a coagulant
- Reaction and flocculation tanks with slow-speed agitators
- Clarifier or dissolved air flotation unit, depending on suspended solids load
- Multimedia filter and activated carbon or ultrafiltration as a polishing step
- Cartridge filter (5–10 micron) as final protection for the membranes
This section is unglamorous and often underestimated. In my experience, roughly 15–20% of the total project cost sits here, and it is the section that determines whether the rest of the plant runs for months or weeks between cleanings. A well-designed pretreatment train is the cheapest insurance you will ever buy.
2. Membrane Concentration
Once the water is clean, the goal is to remove as much permeate as possible before it ever reaches a boiler. For high-salinity feeds, standard RO will not cut it — you need high-pressure RO or disk-tube reverse osmosis (DTRO).
A typical 50 KLD membrane skid includes:
- High-pressure feed pump (up to 90–120 bar for DTRO service)
- Membrane modules — spiral wound for low-fouling streams, DTRO for high-fouling or high-salinity streams
- Energy recovery device if operating pressures exceed 60 bar
- Cleaning-in-place (CIP) skid with heated chemical tanks
- Permeate polishing and monitoring instrumentation
If you want a closer look at how these membranes are specified for tough industrial feeds, the DTRO membrane systems overview is a useful reference. The key number here is recovery. A well-run DTRO stage on a 50 KLD feed can push 70–85% of the volume to clean permeate, leaving only 15–30% as brine for the evaporator. That reduction directly shrinks the evaporator size and the operating cost.
3. Evaporation — MVC or MVR
This is the heart of the plant and the largest single line item. For a 50 KLD ZLD system, you have two realistic choices:
- Mechanical vapor compression (MVC/MVR) — electrically driven, compact, low steam demand, best when power is available and steam is not.
- Multi-effect evaporation — steam driven, uses less electricity but needs a boiler and more plot space.
For most 50 KLD installations, MVC wins on simplicity. A single compressor handles the vapor recompression, and the system runs on electricity alone. Typical power consumption for MVC evaporation sits in the range of 20–40 kWh per cubic meter of distillate, depending on boiling point elevation and the number of stages. That is an indicative range — actual figures depend heavily on the salt concentration and the compressor efficiency.
If you want to understand how the compressor and heat exchanger interact, the MVC evaporator technical page covers the working principle in detail. For feeds with very high scaling potential, a forced-circulation design is usually preferable to a falling-film design, because it keeps solids in suspension and reduces the risk of hard scale on the tube surface.
4. Crystallization and Solids Handling
The last stage turns liquid brine into a solid you can truck away. For a 50 KLD plant, this is usually a small crystallizer or a brine concentrator followed by a cooling crystallizer, plus a dewatering device.
- Forced-circulation crystallizer with vapor compressor
- Slurry transfer pump and holding tank
- Centrifuge or screw press for solid-liquid separation
- Mother liquor return line back to the evaporator
- Solid storage hopper or bagging station
The screw press is often the right choice at this scale. It handles high-solids slurries, runs continuously, and tolerates the abrasive nature of salt crystals better than some centrifuge designs. If you want a deeper look at how screw presses are specified for this duty, the screw press dewatering guide is worth reading before you finalize the solids train.
Cost Breakdown for a 50 KLD ZLD Plant
The table below shows indicative capital cost ranges for a 50 KLD ZLD system treating a moderately saline industrial wastewater. These are ranges, not quotes. Your actual number depends on the feed analysis and the discharge requirements.
| Equipment / Section | Typical CAPEX Range (USD) | Notes |
|---|---|---|
| Equalization and pretreatment | $30,000 – $65,000 | Higher if oil, heavy metals, or high silica present |
| Membrane concentration (RO/DTRO) | $40,000 – $90,000 | DTRO costs more than spiral RO but handles tougher feeds |
| MVC evaporator | $70,000 – $160,000 | Driven by materials of construction and compressor size |
| Crystallizer and solids handling | $25,000 – $60,000 | Depends on whether salt must be sold or landfilled |
| Instrumentation and controls | $15,000 – $35,000 | PLC, HMI, online conductivity and pH |
| Piping, valves, structural, electrical | $20,000 – $50,000 | Site-dependent; containerized skids reduce this |
| Total installed CAPEX | $180,000 – $420,000 | Excludes civil works and site preparation in some cases |
Two things I always tell clients before they look at the total: first, the evaporator is the single biggest line item, and second, the cost of getting the pretreatment wrong is far higher than the cost of over-specifying it. I have seen a plant save $20,000 on pretreatment and then spend $60,000 in the first year on membrane replacements and cleaning chemicals.
Operating Cost — The Number That Actually Matters
CAPEX is a one-time hit. OPEX runs for the life of the plant. For a 50 KLD ZLD system, the dominant operating costs are:
- Electricity — typically 25–45 kWh per m³ of feed, dominated by the MVC compressor and high-pressure pumps
- Chemicals — antiscalant, cleaning agents, pH adjustment, typically $3–8 per m³ of feed
- Membrane replacement — DTRO elements usually last 2–4 years, spiral RO 3–5 years
- Maintenance labor — 4–8 hours per week for routine checks and cleaning
- Solid waste disposal — highly variable; can range from $50 to $400 per ton depending on local landfill or reuse options
If you want a more detailed breakdown of how evaporator operating costs are built up, the MVR evaporator cost analysis covers the price drivers in depth. The short version: electricity price and salt load dominate everything else.
Technology Selection — MVC vs Multi-Effect vs Hybrid
One of the most common questions I get is whether to use MVC or a multi-effect evaporator for a 50 KLD system. The honest answer is that it depends on what you already have on site.
| Factor | MVC / MVR | Multi-Effect |
|---|---|---|
| Steam requirement | None (electric drive) | Requires boiler |
| Electricity demand | High (compressor) | Low |
| Footprint | Compact | Larger, multiple vessels |
| Startup time | Fast | Slower, needs steam warm-up |
| Best fit | No steam available, small footprint | Steam already on site, larger volumes |
For a 50 KLD plant, MVC usually wins on simplicity and footprint. If you already have a boiler and cheap steam, a double- or triple-effect system may have a lower operating cost over a 10-year horizon. The break-even is usually somewhere around the point where steam cost drops below the equivalent electricity cost for compression.
If you are evaluating multi-effect options, the multi-effect evaporator page covers the configuration trade-offs. For most small industrial plants without steam, I lean toward MVC.
Design Details That Decide Whether the Plant Works
Materials of Construction
This is where a lot of projects get into trouble. Chloride-rich brines will destroy 304 stainless steel in months. For high-chloride feeds, you need 2205 duplex, 2507 super duplex, or titanium in the wetted parts of the evaporator. This can add 20–40% to the evaporator cost, but it is not optional. I have seen a 316L heat exchanger fail in under six months on a brine with 40,000 mg/L chloride.
Scaling and Fouling Control
Calcium sulfate, calcium carbonate, and silica are the three most common scale formers in ZLD systems. Silica is the worst because it is difficult to remove chemically once deposited. The two main defenses are:
- Operating the evaporator below the silica saturation point, which limits concentration factor
- Adding a silica removal step (magnesium dosing or lime softening) in pretreatment
If your feed has more than 50 mg/L silica, budget for a removal step. It is cheaper than dealing with a scaled evaporator.
Boiling Point Elevation
As salt concentration rises, the boiling point of the brine increases. This reduces the effective temperature difference across the heat exchanger and increases compressor work. For high-TDS brines, this can add 10–20% to the compressor power. It is one of the reasons a system that looks fine on paper can underperform in the field.
Turn-down and Batch Operation
Many 50 KLD plants do not run continuously. If your plant runs 8 hours a day, the equipment has to handle start-stop cycles without scaling or thermal shock. Forced-circulation evaporators handle this better than falling-film designs. If the plant runs intermittently, specify the control system accordingly.
What I Would Do Differently on the Next Project
After enough of these projects, a few patterns become clear:
- Spend more on pretreatment than you think you need. The cost of a bigger clarifier or an extra filtration stage is small compared to the cost of cleaning a fouled evaporator.
- Get a proper water analysis before you size anything. A single sample is not enough. You need at least a week of composite data, and you need to understand the variability.
- Design for the worst case, not the average. If your feed TDS swings from 2% to 8%, size for 8%.
- Keep the crystallization step simple. At 50 KLD, a forced-circulation crystallizer with a screw press is usually more reliable than a complex multi-stage system.
- Plan for the solid waste. Where does the salt go? If there is no landfill or reuse market, the whole ZLD system becomes a bottleneck.
Maintenance and Common Failure Points
The most common failures I see on 50 KLD ZLD plants are not catastrophic. They are slow degradations that quietly raise operating cost:
- Compressor seal wear — usually shows up as reduced distillate output and higher power draw
- Heat exchanger scaling — detected by rising pressure drop and falling heat transfer
- Membrane fouling — rising feed pressure and falling permeate quality
- Pump cavitation — often from running the evaporator at too low a level
- Instrument drift — conductivity and pH probes need regular calibration, or the control system will make bad decisions
A well-run plant needs about 4–8 hours of operator attention per week. A neglected plant needs a service call every month. The difference is almost entirely in the daily checks and the cleaning schedule.
Frequently Asked Questions
How much does a 50 KLD ZLD plant cost?
For a typical industrial wastewater feed, the installed capital cost ranges from about $180,000 to $420,000. The wide range reflects differences in feed chemistry, materials of construction, and whether the system is skid-mounted or built on site. High-chloride or high-silica feeds push toward the upper end.
What is the power consumption of a 50 KLD ZLD system?
Total power consumption usually falls between 25 and 45 kWh per cubic meter of feed. The MVC compressor is the largest consumer, followed by high-pressure membrane pumps. Actual consumption depends on the salt concentration, boiling point elevation, and the compressor efficiency.
Can I use standard RO instead of DTRO for the membrane stage?
It depends on the feed. If the feed is relatively clean and the TDS is below about 2%, spiral-wound RO can work. For high-salinity, high-fouling, or high-suspended-solids feeds, DTRO is usually the better choice because it handles higher pressures and tolerates more fouling before cleaning.
How often does the evaporator need cleaning?
A well-designed and well-operated MVC evaporator typically needs a chemical clean every 2–6 months. If cleaning is needed more often than that, the pretreatment is probably not doing its job, or the concentration factor is set too high.
What is the biggest mistake in specifying a 50 KLD ZLD plant?
Underestimating the pretreatment requirement. Most of the operational problems I have seen trace back to inadequate removal of hardness, silica, or organics before the water reaches the evaporator. Fixing pretreatment after commissioning is far more expensive than getting it right the first time.
Can a 50 KLD ZLD plant run unattended?
Not fully. It can run with minimal supervision, but it still needs daily checks on levels, pressures, and temperatures, and weekly cleaning or calibration routines. Fully unattended operation is possible only with a robust control system and remote monitoring, and even then, someone needs to respond to alarms.
If you are planning a 50 KLD ZLD system and want to talk through the equipment list and cost drivers for your specific feed, you can reach out to our engineering team. We can review your water analysis and give you a realistic picture of what the plant will look like and what it will cost to run.