

A 100 KLD zero liquid discharge (ZLD) plant is a compact but complete treatment train that takes 100 cubic meters per day of industrial wastewater and turns it into reusable water and a dry solid residue, with no liquid leaving the site. In practice, the design almost always combines pretreatment, membrane concentration, and a thermal evaporator/crystallizer, because no single technology can hit zero discharge on real industrial water. Capital cost typically lands between USD 350,000 and USD 1.2 million depending on salinity, organics, and the evaporation technology you choose, while operating cost is dominated by electricity and thermal energy. This guide walks through the actual design logic, equipment selection, and cost drivers I use when scoping a 100 KLD ZLD system.
What “100 KLD ZLD” Really Means in Engineering Terms
100 KLD means 100 m³/day of feed wastewater, or roughly 4.2 m³/hour if you run 24 hours. That is a small-to-mid industrial scale. It is small enough that a packaged, skid-mounted system makes sense, but large enough that every design decision shows up on the operating budget within the first year.
Zero liquid discharge does not mean “no residue.” It means no liquid discharge. You still produce:
- Reclaimed water (typically 85–95% recovery, project-dependent)
- A concentrated brine that gets evaporated
- A solid salt or mixed salt cake that goes to landfill or a licensed handler
The recovery percentage is the single most important number in the whole design. It drives membrane sizing, evaporator capacity, and the volume of solids you have to manage. I have seen clients assume 95% recovery and then discover their water chemistry caps them at 80%. That gap is a 3x difference in evaporator duty.

Step 1: Characterize the Wastewater Before You Draw Anything
Every failed ZLD project I have reviewed started with incomplete water analysis. You cannot design a 100 KLD ZLD plant from a single sample. You need at least a 30-day composite, plus a spike sample if the plant has batch discharges.
Here is the minimum data set I ask for before quoting:
| Parameter | Why It Matters | Typical Concern Threshold |
|---|---|---|
| TDS / conductivity | Sets membrane recovery and evaporator duty | > 15,000 mg/L pushes you toward thermal-first |
| COD / TOC | Fouls membranes, foams in evaporators | > 2,000 mg/L needs oxidation pretreatment |
| Hardness (Ca, Mg) | Scaling in RO and evaporator tubes | > 200 mg/L as CaCO₃ needs softening |
| Silica | Forms hard scale that is very difficult to remove | > 50 mg/L needs specific antiscalant or precipitation |
| Oil & grease | Destroys membranes and coats heat exchangers | > 10 mg/L needs DAF or coalescer upstream |
| Heavy metals | Can be recovered or must be stabilized in solids | Varies by metal |
| Chloride / sulfate | Corrosion and salt cake composition | Drives material selection |
I want to stress the silica number. Silica is the most common reason a ZLD system underperforms after commissioning. It does not show up in a basic TDS test, and it does not respond to standard antiscalants. If your feed has high silica, budget for a dedicated removal step.
Step 2: Pretreatment — The Part Everyone Underfunds
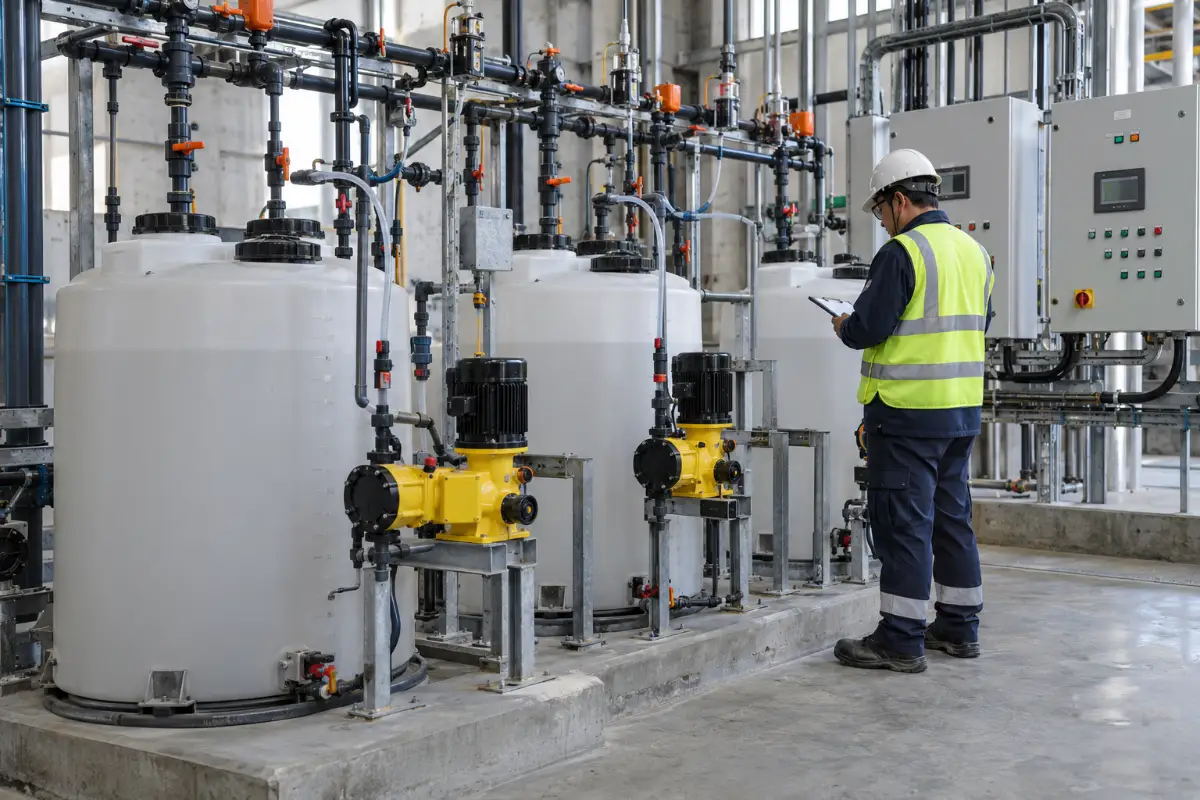
Pretreatment is 20–30% of the capital cost and about 50% of the reliability. Skipping it does not save money; it just moves the cost to downtime.
Typical pretreatment sequence for a 100 KLD ZLD plant
- Equalization tank (8–24 hours retention) to smooth flow and concentration swings
- Chemical softening (lime or caustic + soda ash) if hardness is high
- Coagulation and flocculation followed by clarification or DAF
- Filtration — multimedia, then cartridge or ultrafiltration
- Activated carbon or advanced oxidation if COD is stubborn
- Antiscalant and pH adjustment before membranes
For sludge handling from the softening and clarification steps, a screw press sludge dewatering unit is usually the right call at this scale. It handles variable sludge quality, uses little wash water, and the maintenance is straightforward compared with a filter press.

Step 3: Membrane Concentration — Where the Real Volume Reduction Happens
The economics of ZLD depend on removing as much water as possible before you pay for thermal evaporation. Evaporating water costs roughly 10–20 times more per cubic meter than pushing it through a membrane. So the design goal is simple: concentrate as far as the chemistry allows with membranes, then hand off the minimum volume to the evaporator.
Membrane options at 100 KLD
| Technology | Typical Achievable Concentration | Best Fit |
|---|---|---|
| Standard industrial RO | Up to ~70,000 mg/L TDS | Low-fouling, low-salinity feeds |
| High-pressure RO | Up to ~100,000 mg/L TDS | Brackish concentrates |
| DTRO (disc tube RO) | Up to ~120,000 mg/L TDS | High-fouling, high-salinity, landfill leachate |
For most 100 KLD industrial ZLD projects, I design a two-stage membrane train: standard RO first, then a DTRO membrane system on the RO concentrate. This combination routinely gets the reject volume down to 10–20% of the original feed, which is what makes the thermal stage affordable.
If you need higher pressure capability, a high-pressure RO membrane selection matters more than most people think. Membrane chemistry, spacer design, and element construction all affect how far you can push concentration before fouling forces a cleaning cycle.
Why DTRO keeps showing up in ZLD designs
DTRO handles the water that standard RO cannot: high salinity, high COD, high scaling potential. The open-channel disc design tolerates suspended solids that would plug a spiral-wound element in days. It is not cheap, and the energy demand is higher, but it lets you concentrate further and shrink the evaporator.

Step 4: Thermal Evaporation and Crystallization
This is where the remaining concentrated brine becomes water vapor and solid salt. At 100 KLD feed, the evaporator typically handles 5–20 m³/day of concentrate, depending on upstream recovery.
Choosing between MVC/MVR and multi-effect evaporation
Two families dominate:
- Mechanical vapor compression (MVC/MVR) — uses a compressor to recompress the vapor and reuse its latent heat. Electricity-driven. Compact. Best when power is available and steam is not.
- Multi-effect evaporation (MEE) — uses steam in a cascade of effects. Lower electrical demand but needs a steam supply or a boiler. Larger footprint.
For a 100 KLD plant, MVC/MVR is usually the better fit because it avoids the need for a dedicated steam system and starts up faster. A mechanical vapor compression MVC evaporator at this scale typically consumes 20–40 kWh per cubic meter of distillate, though that number moves a lot with boiling point elevation and compressor type.
Where steam is already available on site, a multi-effect evaporator can cut electrical demand substantially, at the cost of higher thermal energy consumption. The trade-off is site-specific and depends on your energy pricing.
For final crystallization, you either add a forced-circulation crystallizer or use a spray dryer for small volumes. At 100 KLD feed, the salt production is often under 500 kg/day, which is manageable with a single crystallizer.

Step 5: The Cost Breakdown — What Actually Drives the Number
I get asked for a “price for 100 KLD ZLD” almost every week. The honest answer is that the range is wide because the water is different. Here is a realistic indicative breakdown for a 100 KLD industrial ZLD plant.
| System Component | Indicative CAPEX Share | Notes |
|---|---|---|
| Equalization, chemical dosing, softening | 10–15% | Scales with hardness and metals |
| Clarification / DAF + sludge dewatering | 10–15% | Screw press or filter press |
| Filtration and polishing | 5–8% | UF, cartridge, carbon |
| RO + DTRO membrane train | 20–30% | Driven by recovery target |
| MVC/MVR or MEE evaporator | 30–40% | Largest single line item |
| Crystallizer / dryer | 5–10% | Often optional at small scale |
| Instrumentation, controls, skid, piping | 10–15% | Overlaps with all above |
Indicative total CAPEX: USD 350,000 to USD 1,200,000 for a 100 KLD system, project-dependent. A simple, low-salinity feed with high recovery will sit at the bottom. A high-COD, high-silica, high-chloride stream with a crystallizer will sit at the top.
Operating cost drivers
- Electricity — the largest OPEX item if you use MVC/MVR
- Steam or natural gas — dominant if you use MEE
- Membrane replacement — typically every 2–4 years for RO, longer for DTRO
- Antiscalant and cleaning chemicals — small but constant
- Solids disposal — highly variable by region and salt type
- Labor — a well-automated 100 KLD plant can run with part-time attention
For a rough planning number, budget USD 8–25 per cubic meter of feed for total OPEX, again with a wide band because energy price and salt disposal dominate.
Step 6: Materials of Construction and Corrosion
At 100 KLD, you are still dealing with real industrial water. The concentrate at the end of the membrane train can be extremely aggressive.
- Duplex 2205 or 2507 stainless for evaporator wetted parts handling chlorides
- Titanium or high-alloy for the hottest, most concentrated sections
- FRP or PP for low-temperature piping and tanks
- Hastelloy or graphite only where absolutely required — it drives cost fast
I have seen projects save 15% on CAPEX by downgrading materials and then spend that 15% twice over in the first two years on repairs. Chloride stress corrosion cracking does not negotiate.
Step 7: Controls, Automation, and Operator Reality
A 100 KLD ZLD plant should be largely automatic. Operators at small industrial sites wear many hats, and a system that needs constant tuning will not be run correctly.
What I specify as standard:
- PLC-based control with HMI and remote monitoring
- Automatic CIP (clean-in-place) cycles for membranes
- Conductivity and recovery-based flush logic
- Interlocks on evaporator level, temperature, and compressor current
- Trending and alarm logging with at least 90 days of history
Remote diagnostics are not a luxury at this scale. When something goes wrong on a Saturday, being able to see the trend from a laptop saves a service call and a day of downtime.
Common Failure Modes I See on 100 KLD ZLD Plants
1. Scaling in the evaporator
Usually caused by inadequate softening upstream or wrong antiscalant selection. Symptoms: falling distillate rate, rising compressor amps, frequent CIP.
2. Foaming in the evaporator
Common with high-COD or surfactant-containing feeds. Fixed with antifoam dosing or a mechanical foam breaker, but better prevented by removing organics upstream.
3. Membrane fouling and biofouling
Often traces back to insufficient pretreatment or long shutdowns without preservation. DTRO tolerates more, but it is not immune.
4. Compressor vibration or bearing failure
Usually a symptom of liquid carryover or scale on the impeller. Balance and inlet separation matter.
5. Salt cake quality problems
Mixed salts are harder to dispose of than pure salts. If you can separate sodium chloride from sulfate, disposal cost drops significantly.
Design Trade-Offs You Should Decide Before You Buy
| Decision | Option A | Option B | What Tips the Scale |
|---|---|---|---|
| Evaporation technology | MVC/MVR | Multi-effect | Steam availability and electricity price |
| Membrane concentration | Standard RO only | RO + DTRO | Salinity and fouling potential |
| Crystallization | Include crystallizer | Spray dryer or liquid concentrate off-site | Disposal rules and salt volume |
| Automation level | Full remote monitoring | Local PLC only | Operator availability and site remoteness |
| Materials | Duplex stainless | Higher alloy or titanium | Chloride level and temperature |
None of these decisions has a universal right answer. The right answer is the one that matches your water, your site, and your operating team.
A Note on Regulatory Context
ZLD is often driven by discharge limits rather than by a desire to recover water. The U.S. EPA sets effluent guidelines for many industrial categories, and those limits are what force the design in the first place. The World Bank’s environmental, health, and safety guidelines for water and sanitation also give useful benchmarks for what “acceptable discharge” looks like in different industrial contexts. If you are designing to a specific permit, start with the permit, not the technology.
You can review EPA effluent guidelines at epa.gov/eg and the World Bank EHS guidelines at ifc.org. Both are worth reading before you commit to a ZLD scope.
Frequently Asked Questions
How much does a 100 KLD ZLD plant cost?
Indicative CAPEX ranges from about USD 350,000 to USD 1,200,000 depending on feed chemistry, recovery target, and whether a crystallizer is included. Operating cost typically runs USD 8–25 per cubic meter of feed, driven mainly by electricity, steam, and solids disposal.
Can I run a 100 KLD ZLD plant without an evaporator?
Almost never. Membranes alone can concentrate but cannot reach zero liquid discharge because osmotic pressure eventually exceeds practical limits. You need a thermal step to finish the job.
Should I choose MVC/MVR or multi-effect evaporation?
If you have no steam supply, MVC/MVR is usually the practical choice at this scale. If you already have steam and cheap thermal energy, multi-effect can reduce electrical demand. The decision is site-specific and depends on your energy pricing.
How often do membranes need to be replaced?
RO elements typically last 2–4 years with good pretreatment. DTRO elements often last longer because they tolerate more fouling and can be cleaned more aggressively. Actual life depends heavily on feed quality and cleaning discipline.
What causes the most downtime on a 100 KLD ZLD plant?
Scaling and fouling, in that order. Both trace back to pretreatment. If softening, filtration, and antiscalant dosing are correctly designed and maintained, downtime drops sharply.
Can a 100 KLD ZLD plant be containerized or skidded?
Yes. At this scale, most of the system can be built on skids or in containers, which shortens site installation and improves quality control. The evaporator and crystallizer usually ship as separate modules because of size and weight.
What is the footprint of a 100 KLD ZLD plant?
Typically 150–400 m² of process area, depending on whether you include equalization, sludge handling, and a crystallizer. Vertical arrangement and skid design can reduce this significantly.
Do I need a crystallizer for zero liquid discharge?
Strictly, yes — ZLD means no liquid discharge, so the final concentrate must be solidified. In practice, some sites ship concentrated brine off-site for disposal, which is not true ZLD but is sometimes accepted by the permit.
Final Thoughts
Designing a 100 KLD ZLD plant is not about picking the most advanced technology. It is about matching the treatment train to the specific water, energy, and disposal realities of the site. The plants that run well for ten years are the ones where pretreatment was over-designed rather than under-designed, where membrane concentration was pushed as far as the chemistry allowed, and where the evaporator was sized with a real margin instead of a hopeful one.
If you are scoping a project and want a second opinion on the process train before you commit to equipment, that conversation is usually cheaper than a redesign later.